3-5 Star Guestroom FF&E
Luxury Solid Wood Hotel Bedroom Furniture Set for 3-5 Star Hotels Apartments
Modern Custom
OEM Supply
10-Yr Warranty
View Specifications
Explore contract-grade hospitality furniture manufactured under strict structural engineering standards, designed to meet the rigorous wear criteria of international luxury hotel flags, multi-family high-rises, and turnkey resort developments.
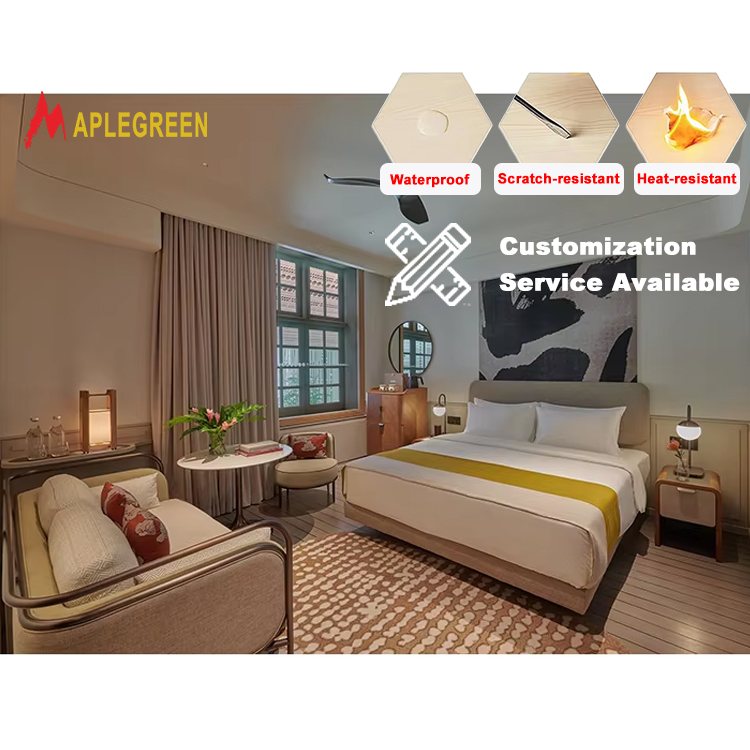

Procuring wooden hotel bedroom sets from China requires an engineer's precision rather than a standard furniture catalog selection. Within commercial hospitality environments, guestroom casegoods, headboard wall assemblies, nightstands, writing credenzas, and luggage consoles undergo intense physical abuse, thermal shifts from localized climate control, and exposure to industrial cleaning chemical agents. A residential furniture mindset inevitably results in delamination, veneer bubbling, and joint failure within two to three operational years.
Direct Chinese manufacturers specializing in five-star FF&E procurement implement strict material composites. The ideal architectural configuration combines a kiln-dried solid hardwood frame (FAS Grade White Oak, Ash, Walnut, or Beech stabilized at 8%–12% equilibrium moisture content) with high-density E0 or E1 substrate panels (MDF or multilayer marine-grade plywood) overlaid with 0.6mm natural quarter-cut wood veneers. This composite construction mitigates natural hygroscopic expansion and contraction, preventing structural warping while delivering the authentic tactile warmth and luxury expected by discerning guests.
Furthermore, structural joinery represents the primary technical discriminator. Contract-grade casegoods mandate machine-cut mortise-and-tenon or heavy dowel joinery reinforced with solid hardwood corner blocks that are glued and corner-screwed. Drawers must utilize English dovetail joints, full-extension concealed soft-close undermount runners rated for a minimum of 50,000 operational cycles, and 12mm solid plywood drawer bottoms to effortlessly withstand luggage impact.
How global brand standards, ESG obligations, and smart-room integration are reshaping hotel furniture manufacturing specifications across China's supply chains.
Hoteliers are rapidly pivoting to floor-to-ceiling modular headboard wall panels integrated with French cleat mounting. This accelerates site installation by up to 45%, isolates acoustic reverberation between guest suites, and facilitates clean housekeeping access under floating nightstands.
Modern bedroom casegoods no longer treat electrical integration as an afterthought. Leading Chinese fabricators now route pre-engineered wire management raceways directly into headboards, writing desks, and credenzas, integrating flush-mount USB-C PD, Qi charging surfaces, and touchless dimmable perimeter lighting.
Driven by strict corporate ESG targets and LEED / WELL certifications, hospitality purchasing agents prioritize suppliers utilizing waterborne polyurethane sealers, UV-curable natural plant lacquers, and formaldehyde-free resin bonds that exceed California Air Resources Board (CARB-P2) and EU standards.
The manufacturing ecosystem in Foshan, Guangdong has transformed dramatically from manual carpentry workshops into world-class digital production ecosystems. Today, best-in-class manufacturers deploy 5-axis CNC machining centers, automated computerized panel nesting, precision linear edge-banding systems, and positive-pressure automated dust-free spray painting lines. This level of automated capital investment eliminates human inconsistency across 500+ room batch runs, ensuring that drawer reveals, veneer woodgrain matching, and hardware recesses align down to 0.2mm engineering tolerances.
| Technical Parameter | Standard Residential Grade | Commercial 4-5 Star Hospitality Grade (Daski Standard) |
|---|---|---|
| Wood Moisture Content (MC) | 14% - 18% (Prone to cracking under HVAC) | 8% - 12% Controlled via Kiln Drying & Moisture Balancing Rooms |
| Substrate Core Panel | Low-density particle board (E2 grade) | High-density CARB-P2 / E0 Multi-layer Birch Plywood or Moisture-Resistant MDF |
| Veneer Thickness & Edge | 0.1mm - 0.2mm paper foil or paper-backed veneer | 0.6mm natural hardwood veneer + 2.0mm solid wood impact-resistant edge banding |
| Surface Coating System | Single coat NC nitrocellulose lacquer | Multi-coat UV/PU polyurethane system, scratch-resistant, alcohol- and stain-proof |
| Drawer Mechanics | Side-mounted ball bearing slides (10k cycles) | Concealed heavy-duty undermount synchronized soft-close slides (50k+ cycle certified) |
| Upholstery Fire Rating | Standard domestic untreated fabrics | Mandatory CAL TB 117 (USA) / BS 5852 Crib 5 (UK) fire retardant foam & fabrics |
Operating a dedicated 28,000 square meter manufacturing plant with full vertical integration from shop drawings to export logistics.
Founded in 2004 in Jiujiang, Foshan, our production footprint houses advanced automated woodworking lines, veneer hydraulic hot-pressing, precision metal laser profiling, and clean finishing facilities operated by 200+ master craftsmen.
Our dedicated hospitality engineering drafting department reviews client architectural elevations, develops detailed 1:1 CAD shop drawings, and proposes value-engineering optimizations to slash budget deficits without compromising design intent.
We eliminate sourcing guesswork by fabricating a 1:1 scale guestroom mock-up in approximately 20 days. Owners, general managers, and interior designers can physically inspect ergonomics, veneer sheen, lighting ambiance, and joinery integrity before batch production.
Fully compliant with US CAL TB 117, British BS 5852 Crib 5 flammability protocols, and European E0/E1 formaldehyde limits. All raw foam, treated upholstery, adhesives, and coatings are tested and verified by independent testing bodies including SGS.
Every casegood piece is protected by thick EPE foam, corner buffer angles, and heavy-duty 5-ply export corrugated shipping cartons. Crates are clearly color-coded and labeled by building floor and guestroom number, drastically reducing on-site handling overhead.
We deploy senior engineering supervisors directly to overseas project sites in North America, Europe, Southeast Asia, and the Middle East to lead local labor teams, ensure architectural alignment, and conduct final punch-list handovers with the hotel operator.
Essential guidance on minimum order quantities, manufacturing lead times, quality assurance milestones, and customs shipping compliance.
For custom commercial hotel bedroom sets, our standard MOQ starts from 10 to 20 guestroom sets, allowing boutique hotel developers and apartment operators to access bespoke manufacturing pricing. For restaurant dining chairs, bar stools, and modular booth seating, typical order minimums start at 20 units. Full-scale single-piece samples and mock-up guestroom suites can be fabricated prior to executing mass purchase agreements.
Our standard production lifecycle is divided into clear accountable milestones: (1) CAD shop drawing engineering: 5 to 10 working days; (2) 1:1 scale guestroom sample mock-up fabrication: approximately 20 days; (3) Mass manufacturing execution: 45 calendar days following client sample room sign-off and deposit confirmation. We also maintain buffer capacity to accommodate multi-phase phased openings.
Wood warping is universally caused by unmanaged equilibrium moisture content (EMC). Before cutting, all raw solid lumber and substrate panels are seasoned in computerized temperature- and humidity-controlled drying kilns until moisture stabilization reaches 8%–12% (custom calibrated to the target delivery country's climate zone). Furthermore, cross-grain balancing veneers and 6-sided moisture seal coats are applied to block ambient humidity ingress.
Yes. Over our 20+ years of operational history, we have successfully fabricated turnkey guestroom packages aligning with brand standard matrices for major hotel groups including Marriott, Hilton, IHG, Wyndham, and Accor. We precisely cross-reference specified wood stains, metal plating sheens, fabric rubs (Wyzenbeek / Martindale 50k+), and electrical outlet cutouts.
Our ISO 9001 quality assurance regimen includes: (1) Raw material incoming inspection (lumber density, veneer grade, board emissions); (2) Pre-assembly fit testing of every room type at our Foshan facility with video documentation; (3) Multi-point hardware functional testing; and (4) Third-party inspection access for SGS, Intertek, or client-nominated QA inspectors prior to container stuffing.
We provide full English-language CAD installation schematics, exploded 3D joinery diagrams, and labeled fastener kits for every unit. Upon request, our senior engineering supervisors travel to the jobsite to manage unpacking, leveling, wall anchoring, and punch-list resolutions. All solid wood commercial hotel bedroom casegoods carry a comprehensive 10-year structural warranty.