Featured Commercial Hotel Bed Suites & Guestroom Packages
Factory-direct OEM/ODM bedroom systems engineered with E0/E1 low-emission substrates, moisture-sealed structural joinery, and architectural integrated wall paneling.
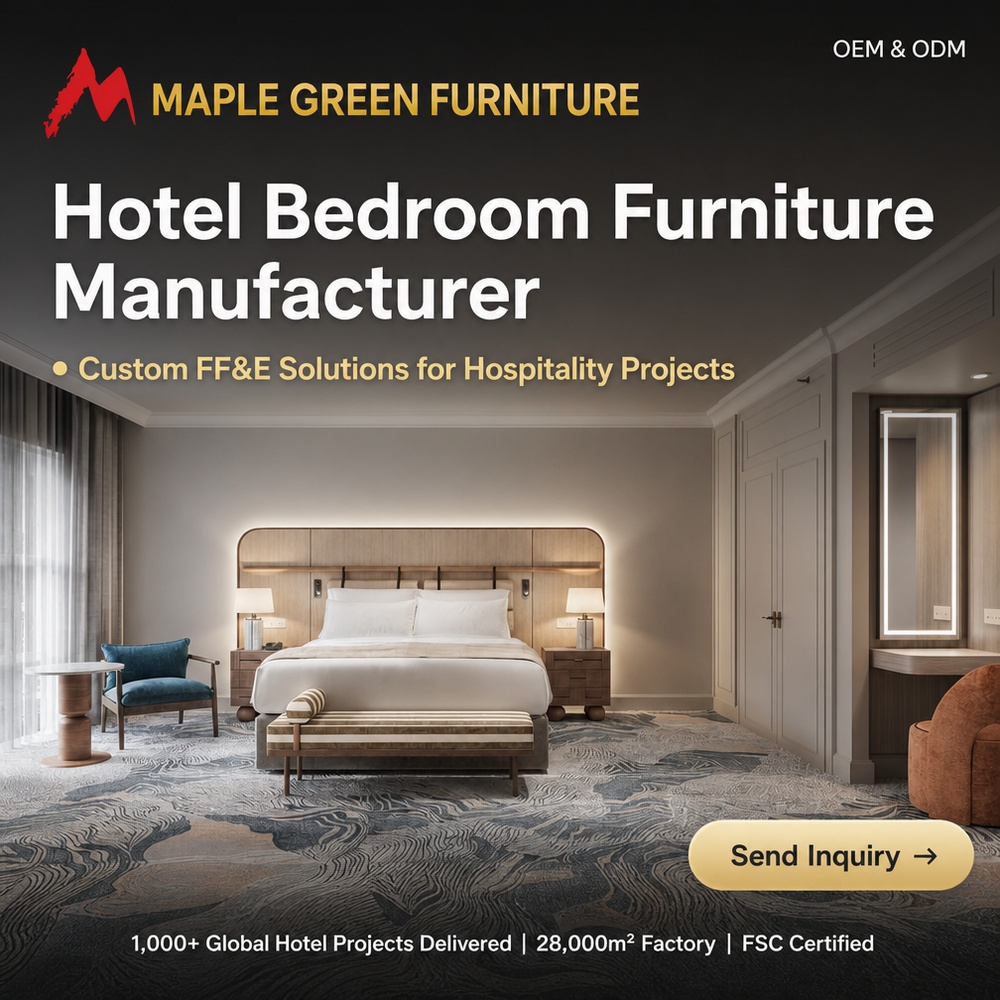
Luxury Hotel Bedroom Furniture Set OEM ODM Custom Modern Design Wood Apartment 5 Star Supplier Manufacturer
- Solid Wood Core + Quarter-Cut Veneer
- Heavy Commercial Load Rating (500kg+)
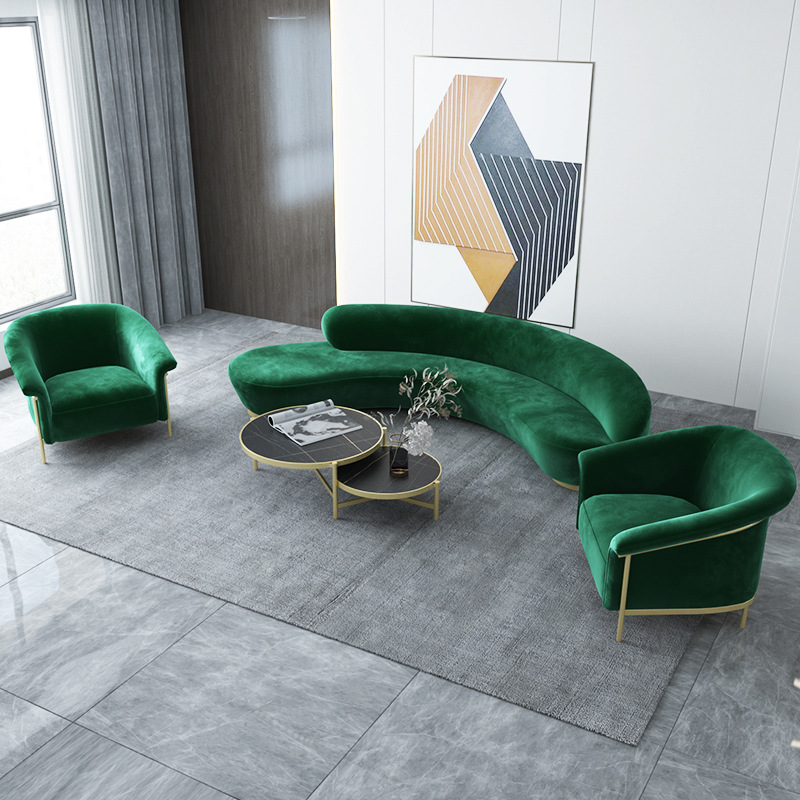
Luxury Club Hotel Lobby Sitting Room Sofa Beauty Salon Rest Area Living Room Reception Hotel Furniture Flannelette Curved Sofa
- High-Density FR Sponge (CAL TB 117)
- Solid Hardwood Kiln-Dried Internal Frame
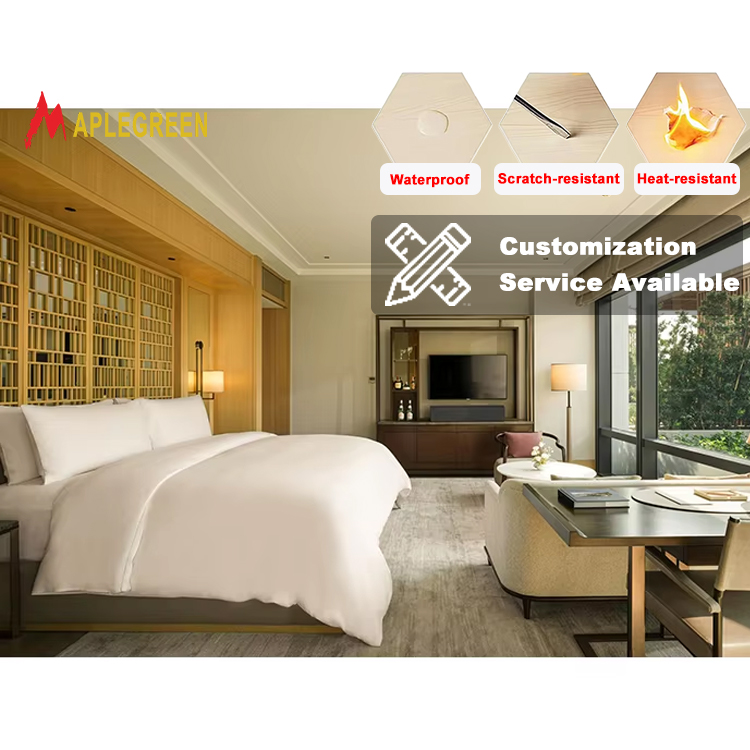
Modern Design Custom Solid Wood Hotel Bedroom Furniture Sets with Leather Slats for Apartment & Villa Use
- Noise-Free Acoustic Slat Integration
- Anti-Scratch Multi-Layer PU Lacquer Finish
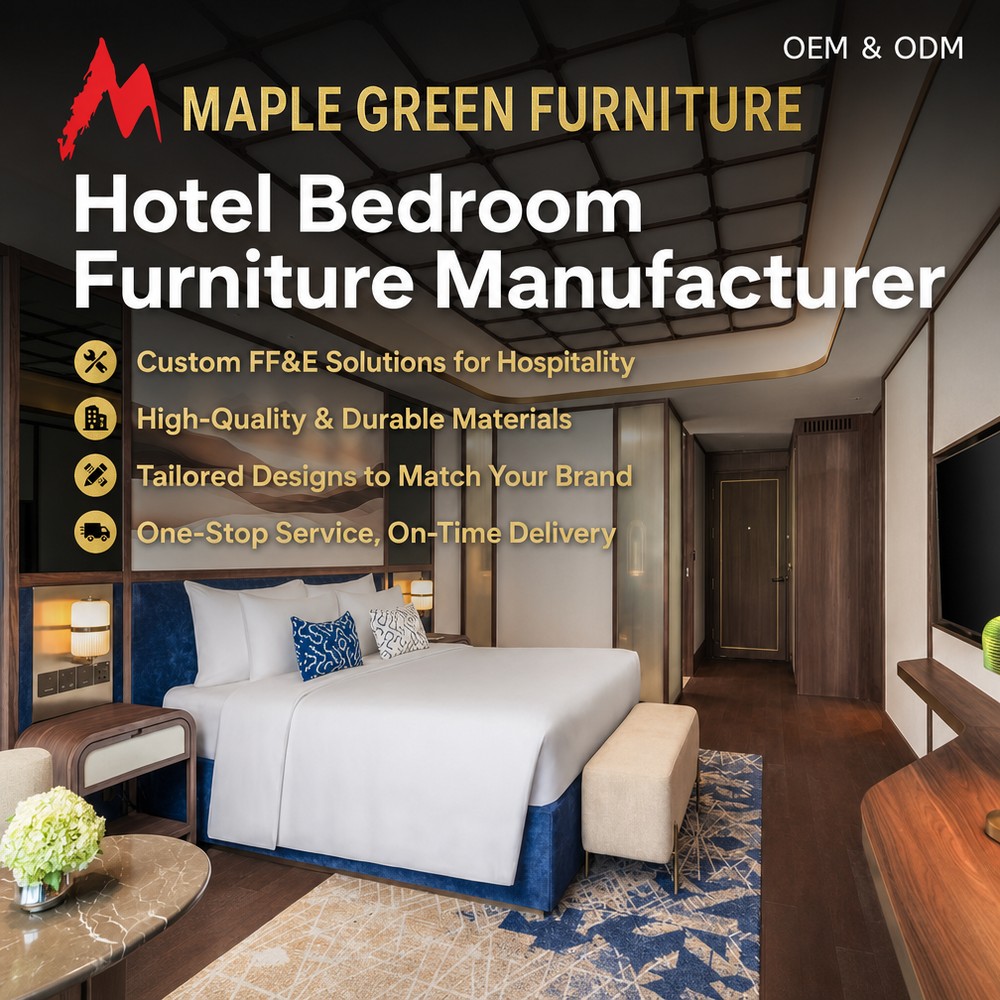
Modern Solid Wood Hotel Bedroom Furniture Set for Apartment and Motel 6 Luxury 5 Star Customizable Commercial Furniture
- High-Traffic Impact-Resistant Edging
- Modular Knock-Down System for Low Freight
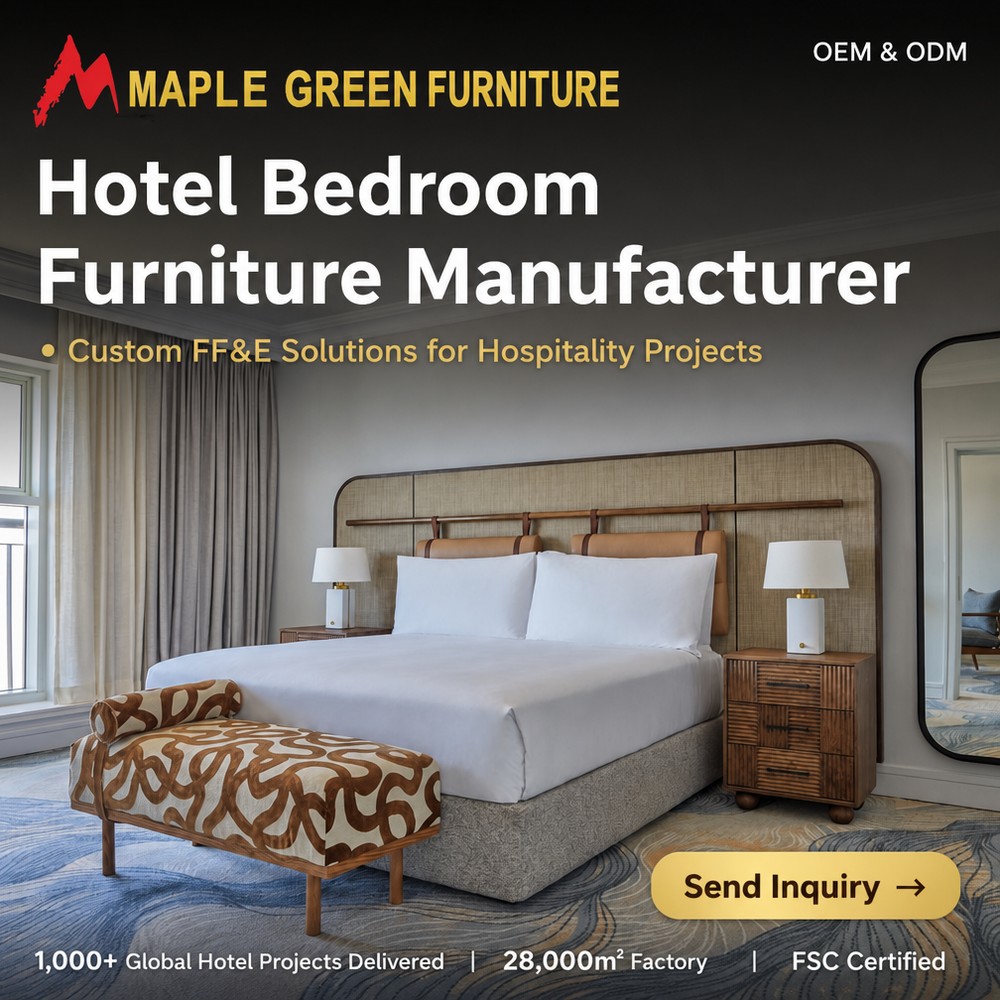
Luxury Solid Wood Eco-Friendly Fire Retardant Hotel Bedroom Furniture Set Turnkey Project Custom Modern Design Apartment Use
- E0 Low-Formaldehyde Hospitality Grade
- BS 5852 Crib 5 Flame Retardancy Cert
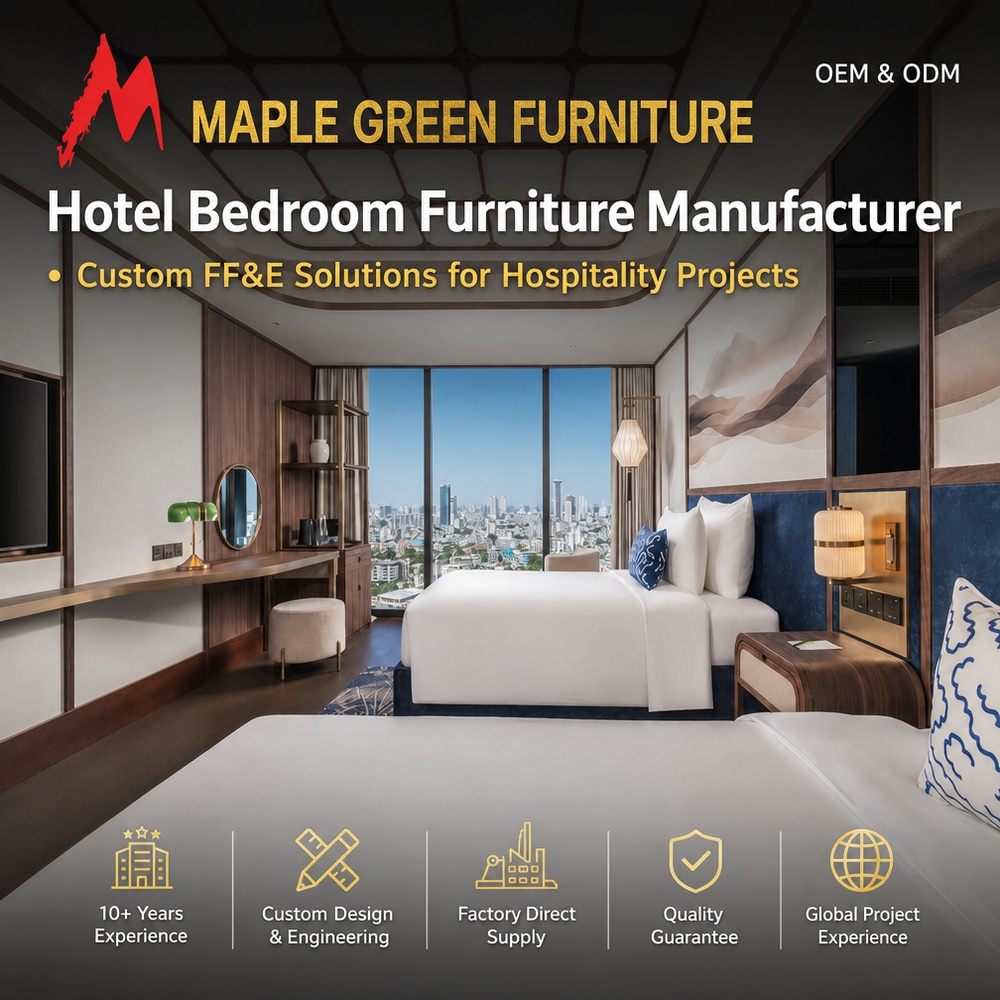
Hotel Bedroom Furniture Set for 5 Star Hotels-Custom Modern Solid Wood Eco-Friendly Luxury Design with 10 Year Warranty
- 10-Year Structural Commercial Warranty
- CNC Concealed Cable Management Ports
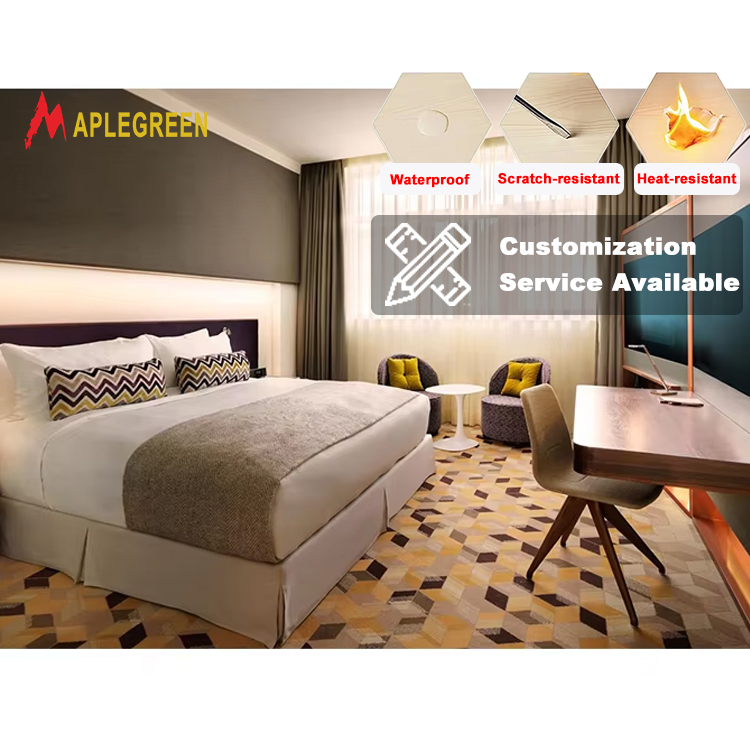
Modern Custom Solid Wood Hotel Bedroom Furniture Sets for 5 Star Luxury Apartments & Villas
- Natural Oak/Walnut Custom Veneers
- Precision Concealed LED Headboard Channels
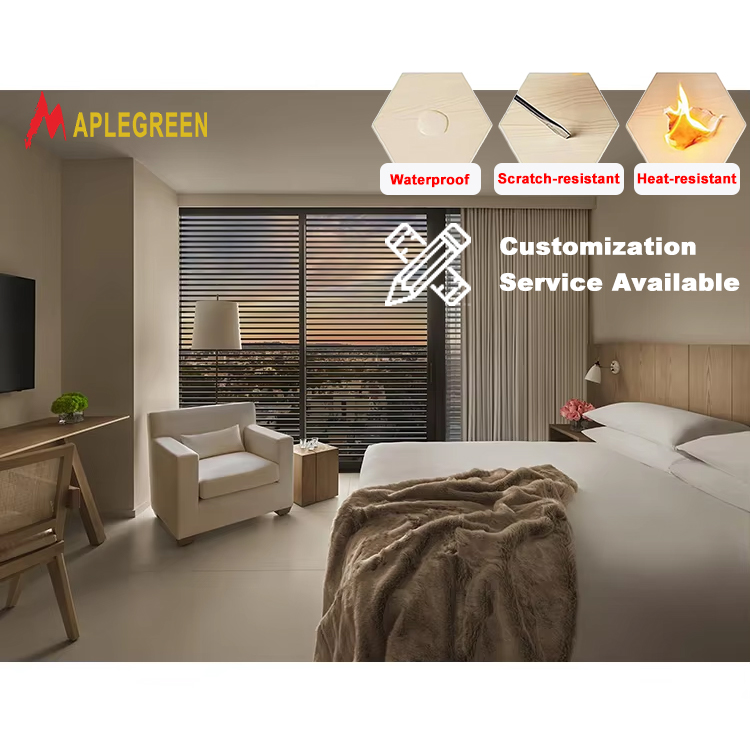
Modern Wood Hotel Bedroom Set with MDF Panel Design Eco-Friendly & Water Resistant for Apartment Villa Use-Commercial Furniture
- Hydrophobic HMR/MDF Internal Core
- UV-Cured Anti-Discoloration Topcoat
Engineering & Manufacturing Standards for Commercial Hotel Beds
Unlike residential furniture, wooden hotel beds endure nonstop turnover, chemical housekeeping agents, fluctuating regional humidity, and rigorous municipal safety audits. Below is the structural baseline enforced by top Chinese OEM suppliers.
Structural Framework & Joinery
Frames utilize kiln-dried solid hardwood (moisture content stabilized at 8%–12%) combined with high-grade multi-layer plywood cores. Mortise-and-tenon joints reinforced with cold-rolled steel corner plates eliminate squeaking and withstand repetitive lateral loads.
Fire-Retardant Standards
Upholstered headboards and integrated wall slats strictly comply with North American CAL TB 117-2013 and British Standard BS 5852 Crib 5 testing, preventing flame propagation and excessive toxic smoke generation in hospitality spaces.
Low-VOC & Formaldehyde Baselines
Meeting EN 717-1 (E0/E1) and CARB Phase 2 compliance, all panel adhesives and finishing lacquers utilize water-based or UV-cured polyurethanes, allowing fast room turnarounds after handover without hazardous chemical outgassing.
| Evaluation Parameter | Commercial Grade (3-Star & Boutique) | Luxury Hospitality Grade (5-Star & Luxury Resorts) |
|---|---|---|
| Frame Material | Solid Birch / Pine Interior + E1 CARB MDF Panels | Kiln-Dried FAS White Ash / Oak + 18mm Marine Plywood Substrate |
| Veneer Spec & Application | 0.4mm Natural Walnut / Engineered Wood Veneer | 0.6mm–2.0mm Quarter-Cut Crown Hardwood Veneer, Hot-Pressed |
| Hardware & Connectors | Concealed Zinc Alloy Eccentric Cam Fittings | Hafele / Blum Heavy-Duty Concealed Fittings + Solid Steel Corner Bracing |
| Surface Protection | Standard Acid-Curing / PU Spray Finish (2H Hardness) | UV-Cured Multi-Coat Polyurethane + Scratch & Alcohol Resistant Topcoat (3H) |
| Fire Compliance | CAL TB 117 / NFPA 260 Core Padding | BS 5852 Crib 5 certified fabric, interliner, and combustion-modified foam |
Future Procurement Trends for Hospitality Wooden Beds (2025–2030)
As global hotel chains revamp design language and prioritize lifecycle sustainability, wooden bed manufacturing is transitioning from stand-alone bedstead fabrication to unified architectural guestroom wall ecosystems.
Integrated IoT & Low-Voltage Millwork
Modern luxury bedframes incorporate flush CNC cutouts for wireless charging stations, capacitive touch dimming, circadian concealed LED glow-strips, and universal Type-C fast chargers built directly into solid wood ledger rails.
Circular FF&E & Modular Replacement
Developers demand field-serviceable assemblies. When edge bands or upholstery scuff, modular bolt-on headboard segments allow maintenance crews to swap parts in under 15 minutes without dismantling the structural wood platform.
FSC Chain of Custody & Carbon Neutrality
Institutional operators require Chain-of-Custody (CoC) documentation for all lumber. Traceable European beech, American white oak, and certified bamboo composites are replacing uncertified hardwoods to meet LEED and BREEAM certifications.
Foshan Daski Furniture: 20+ Years Direct Manufacturing Capacity
Headquartered in Jiujiang, Foshan—China's global center for high-end hospitality casegoods and FF&E manufacturing—we provide unmatched turnkey engineering from shop drawings to on-site assembly.
Shop Drawings in 5–10 Days
Our 20+ member in-house technical detailing team translates conceptual ID renderings into precise AutoCAD and BIM shop drawings with full joint details, material breakdowns, and MEP clearances in under 10 business days.
1:1 Mockup Guestrooms in 20 Days
Before launching mass runs, we build fully functional 1:1 guestroom mockups inside our 2,000 m² project showroom, allowing property owners, procurement agents, and brand inspectors to verify ergonomic clearance, tone, and joinery.
SGS-Assessed & ISO 9001 Certified
Our 28,000 m² production base operates under ISO 9001 quality assurance with incoming raw material moisture tracking, CNC machining accuracy tolerances within ±0.5mm, and individual export-grade carton packaging labelled by room and floor.
Hotel Wooden Bed Procurement FAQ
Common engineering and commercial inquiries from overseas general contractors, interior designers, and hotel procurement consultants.
For custom guestroom bed packages, our baseline production run typically begins at 10 to 20 keys (sets). We readily produce single-piece prototypes and full 1:1 sample room configurations for brand approval prior to authorizing full volume production.
We control wood moisture equilibrium at 8%–12% using computerized kiln chambers calibrated to the destination market's relative humidity (e.g., lower equilibrium for GCC arid zones, higher for Southeast Asia). All solid edges are fully encapsulated with polyurethane sealing coats.
Yes. We regularly build to international brand matrix requirements, matching exact veneer cuts, sheen percentages (typically 15%–30% open/closed pore), integrated LED drivers, and fire retardancy standards such as CAL TB 117 and BS 5852 Crib 5.
Submittal drawings require 5 to 10 days; 1:1 room mockups take approximately 20 days; mass production requires standardly 45 days after finish and shop drawing sign-offs. Staggered batch container shipments are coordinated for phased construction sites.
Ready to Engineer Your Hospitality Bed Packages?
Send us your BOQ (Bill of Quantities), interior design elevation drawings, or sample swatches. Our hospitality engineering team will provide a competitive factory quotation with detailed shop drawing submittals.
Get a Quote