2004
Established in Foshan
28,000m²
Production Complex
1,000+
Projects Installed Worldwide
45Days
Standard FF&E Turnaround
Direct Factory Collection
Engineered Hospitality Guestroom Packages & Casegoods
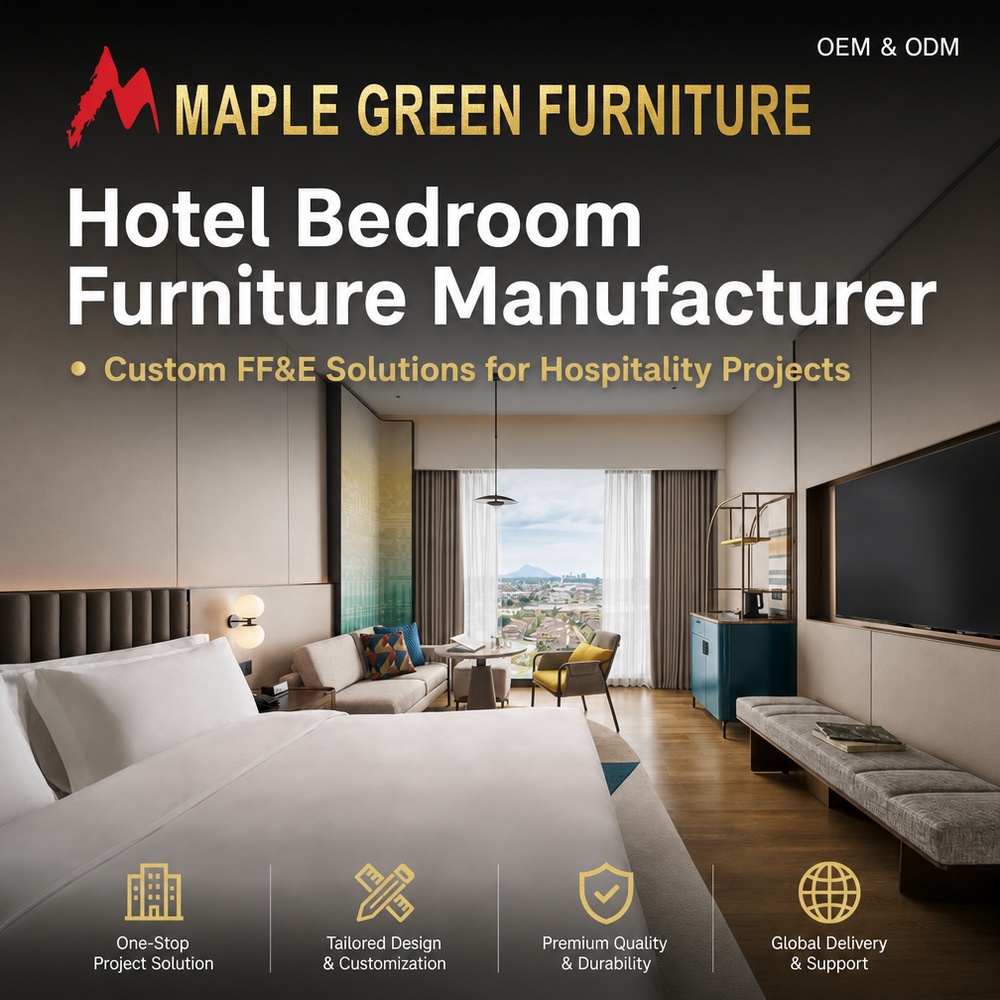
Tested commercial configurations designed for luxury resorts, branded corporate portfolios, boutique developments, and high-density apartments.
Hospitality Procurement Trends
Future-Proofing Hotel Guest Room FF&E: Strategic Procurement Outlook
The international hospitality landscape has moved definitively from transient surface styling toward long-lifecycle modular engineering. Hotel owners, procurement directors, and technical service consultants evaluate furniture packages based on durability, operational flexibility, and adherence to environmental directives.
1. Modular Architectural Integration
Modern guestroom designs eliminate freestanding, disjointed casework in favor of continuous architectural millwork. Integrating acoustic headboard systems, bedside cantilevered desks, concealed wiring chases, and LED task illumination directly into the panel assemblies minimizes site installation labor while ensuring clean sightlines.
2. Decarbonization & Circular Substrates
Low-carbon certifications have evolved from optional marketing bullet points to non-negotiable tender prerequisites. European and North American brand operators systematically require certified E0 or ultra-low emission boards (CARB P2), low-VOC polyurethanes, and verifiable chain-of-custody timber sourcing.
3. High-Turnover Lifecycle Durability
Luggage abrasion, chemical sanitizers, and guest misuse drive premature wear. Procurement strategies emphasize solid hardwood internal edge banding beneath real wood veneers, high-pressure compact laminates for horizontal tops, and fabrics rated above 50,000 Martindale double rubs.
Engineering Standards
Commercial Specifications & Quality Architecture
Standardizing cross-border hospitality manufacturing requires strict adherence to international safety metrics, flammability thresholds, and load tolerances.
| Component Package | Material Specification | Compliance & Test Metric | Operational Engineering Benefit |
|---|---|---|---|
| Substrates & Panels | Moisture-resistant E0/E1 MDF, multi-layer solid birch plywood core | CARB Phase 2 / EN 120 / ISO 9001 | Prevents warping in tropical and air-conditioned guest room fluctuations. |
| Upholstery Foam | High-resilience memory composite (density 45–60 kg/m³) | CAL TB 117 (USA) / BS 5852 Crib 5 (UK) | Flame-retardant performance without structural sagging over 10-year usage. |
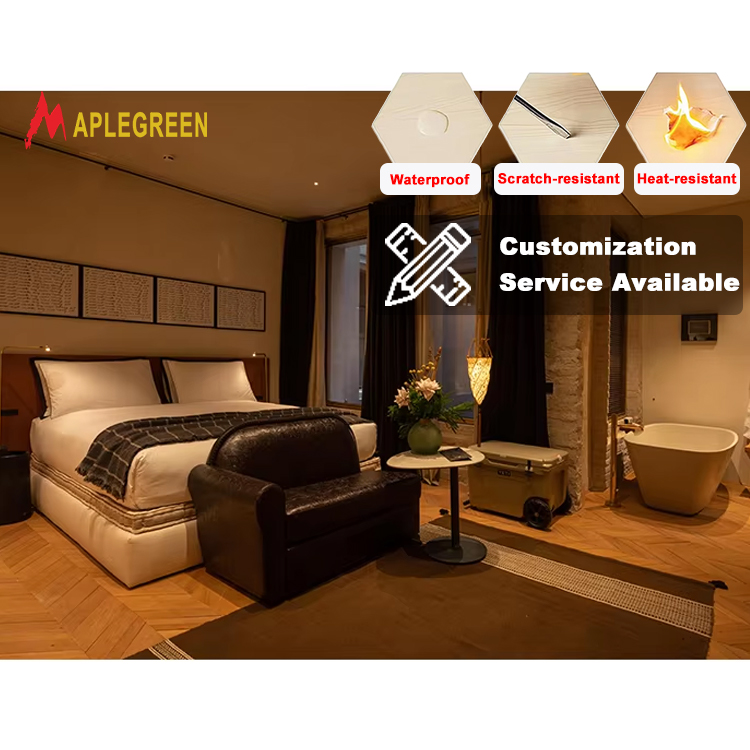
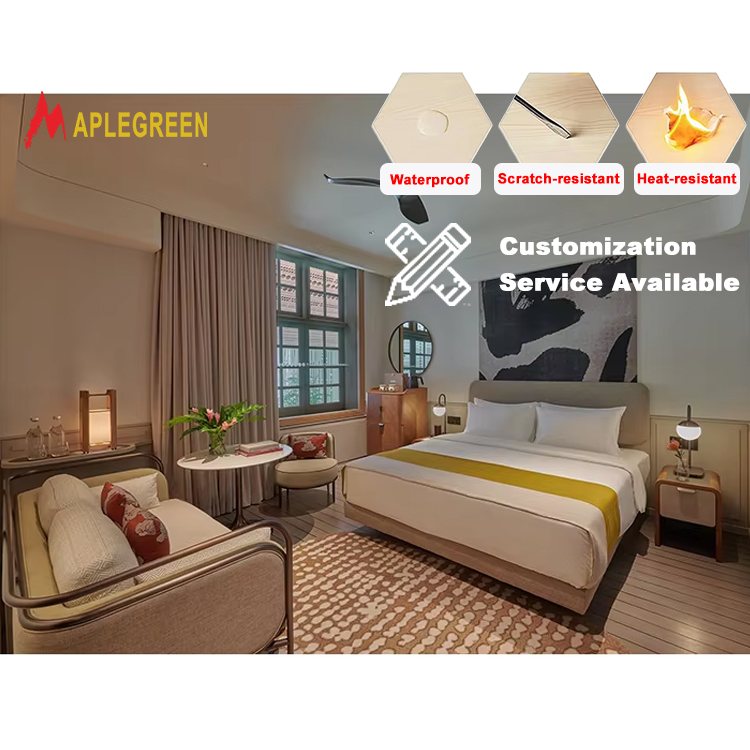
| Surface Finishes | Quarter-cut natural oak/walnut veneer + PU multi-coat seal | ASTM D3363 3H Pencil Hardness / Scratch Tested | High resistance to hot beverage rings, alcohol-based cleansers, and impact. |
| Hardware Joinery | Concealed soft-close undermount slides, DTC/Blum dampers | ANSI / BIFMA X5.5 Standard 50,000 cycle test | Eliminates acoustic impact in adjacent rooms and guarantees smooth drawer glide. |
Direct Factory Infrastructure
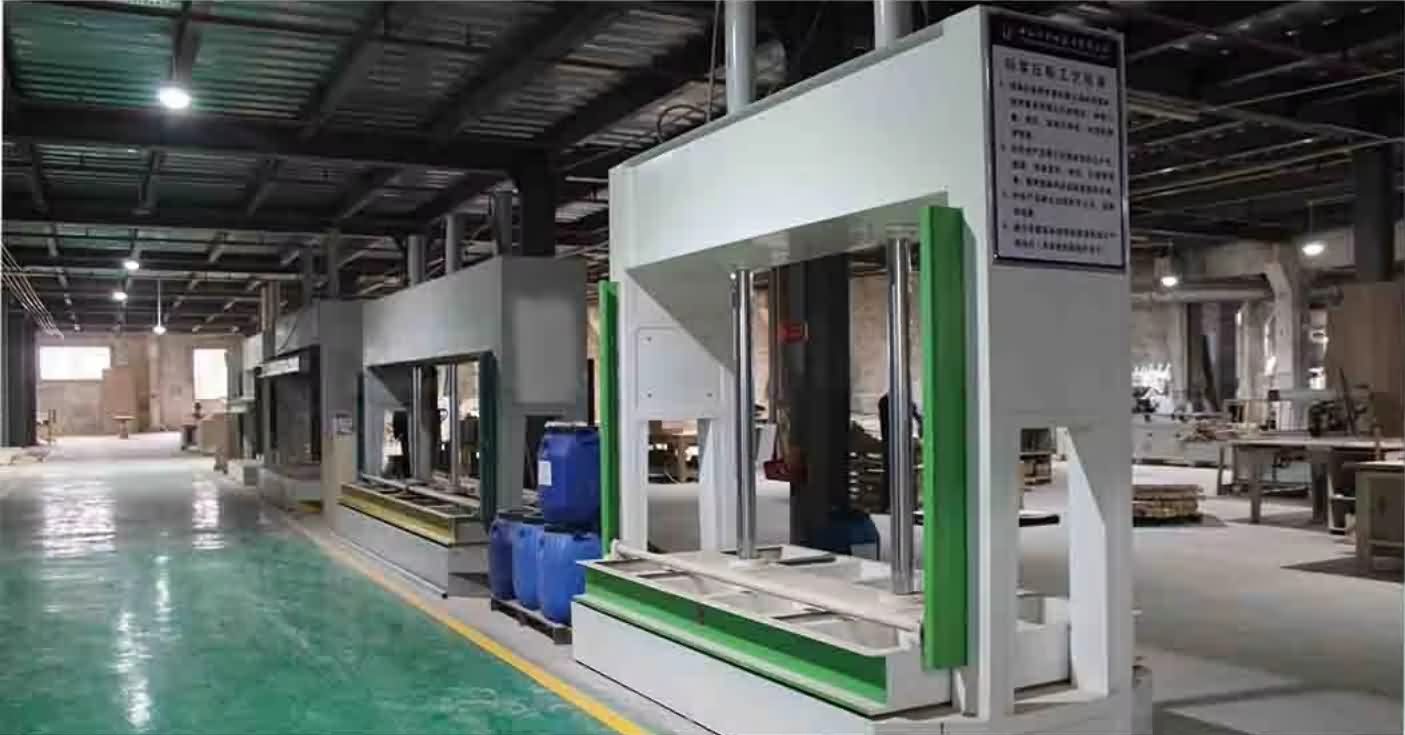
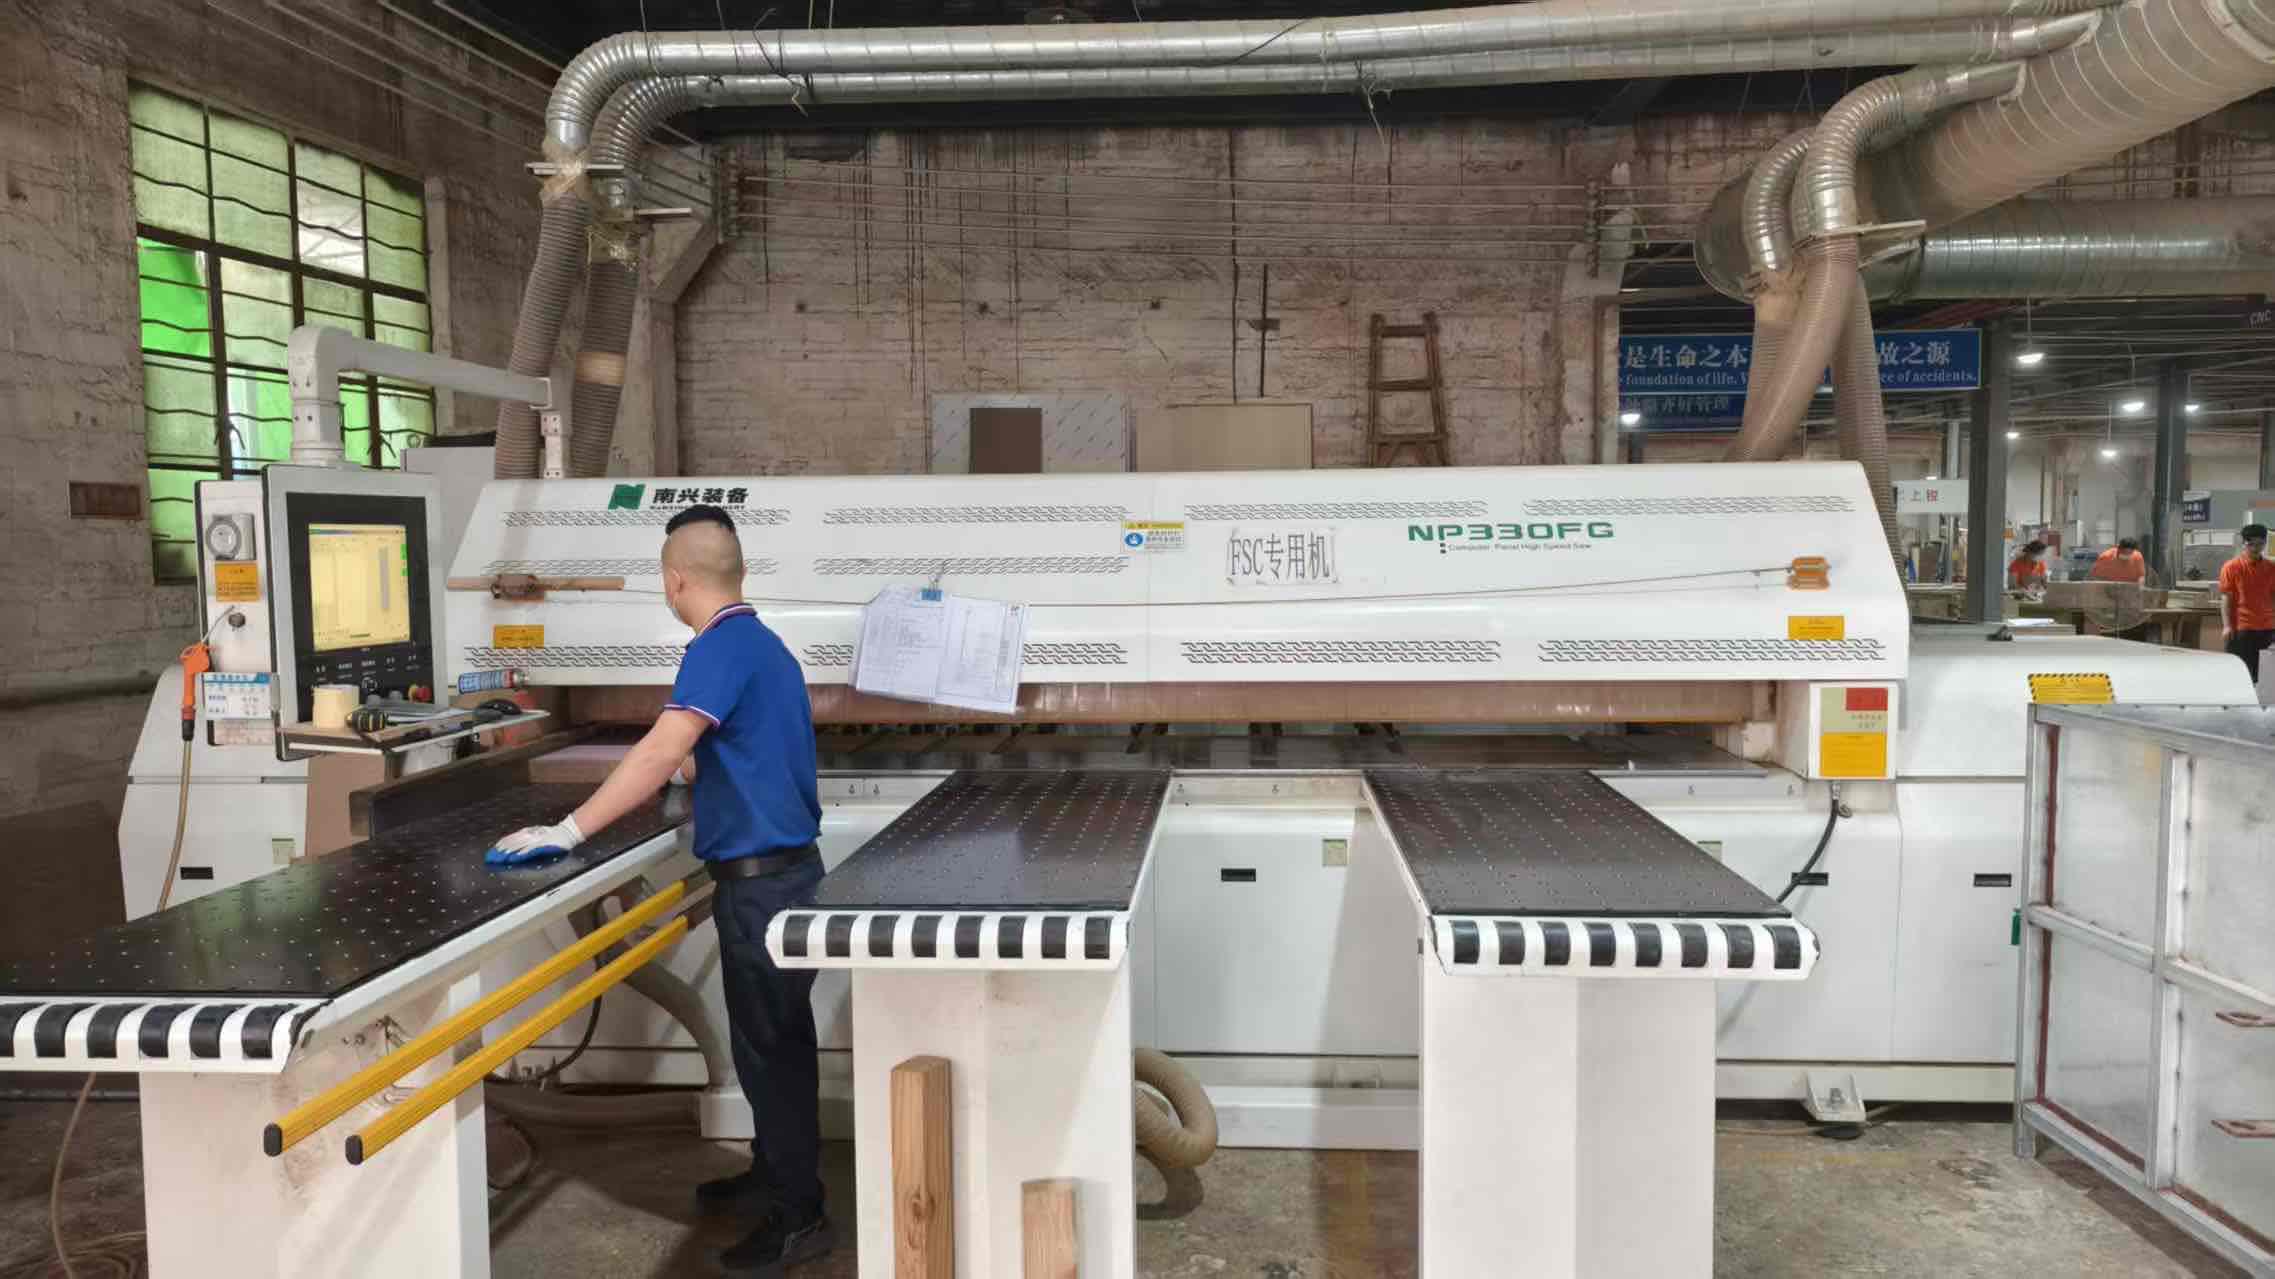
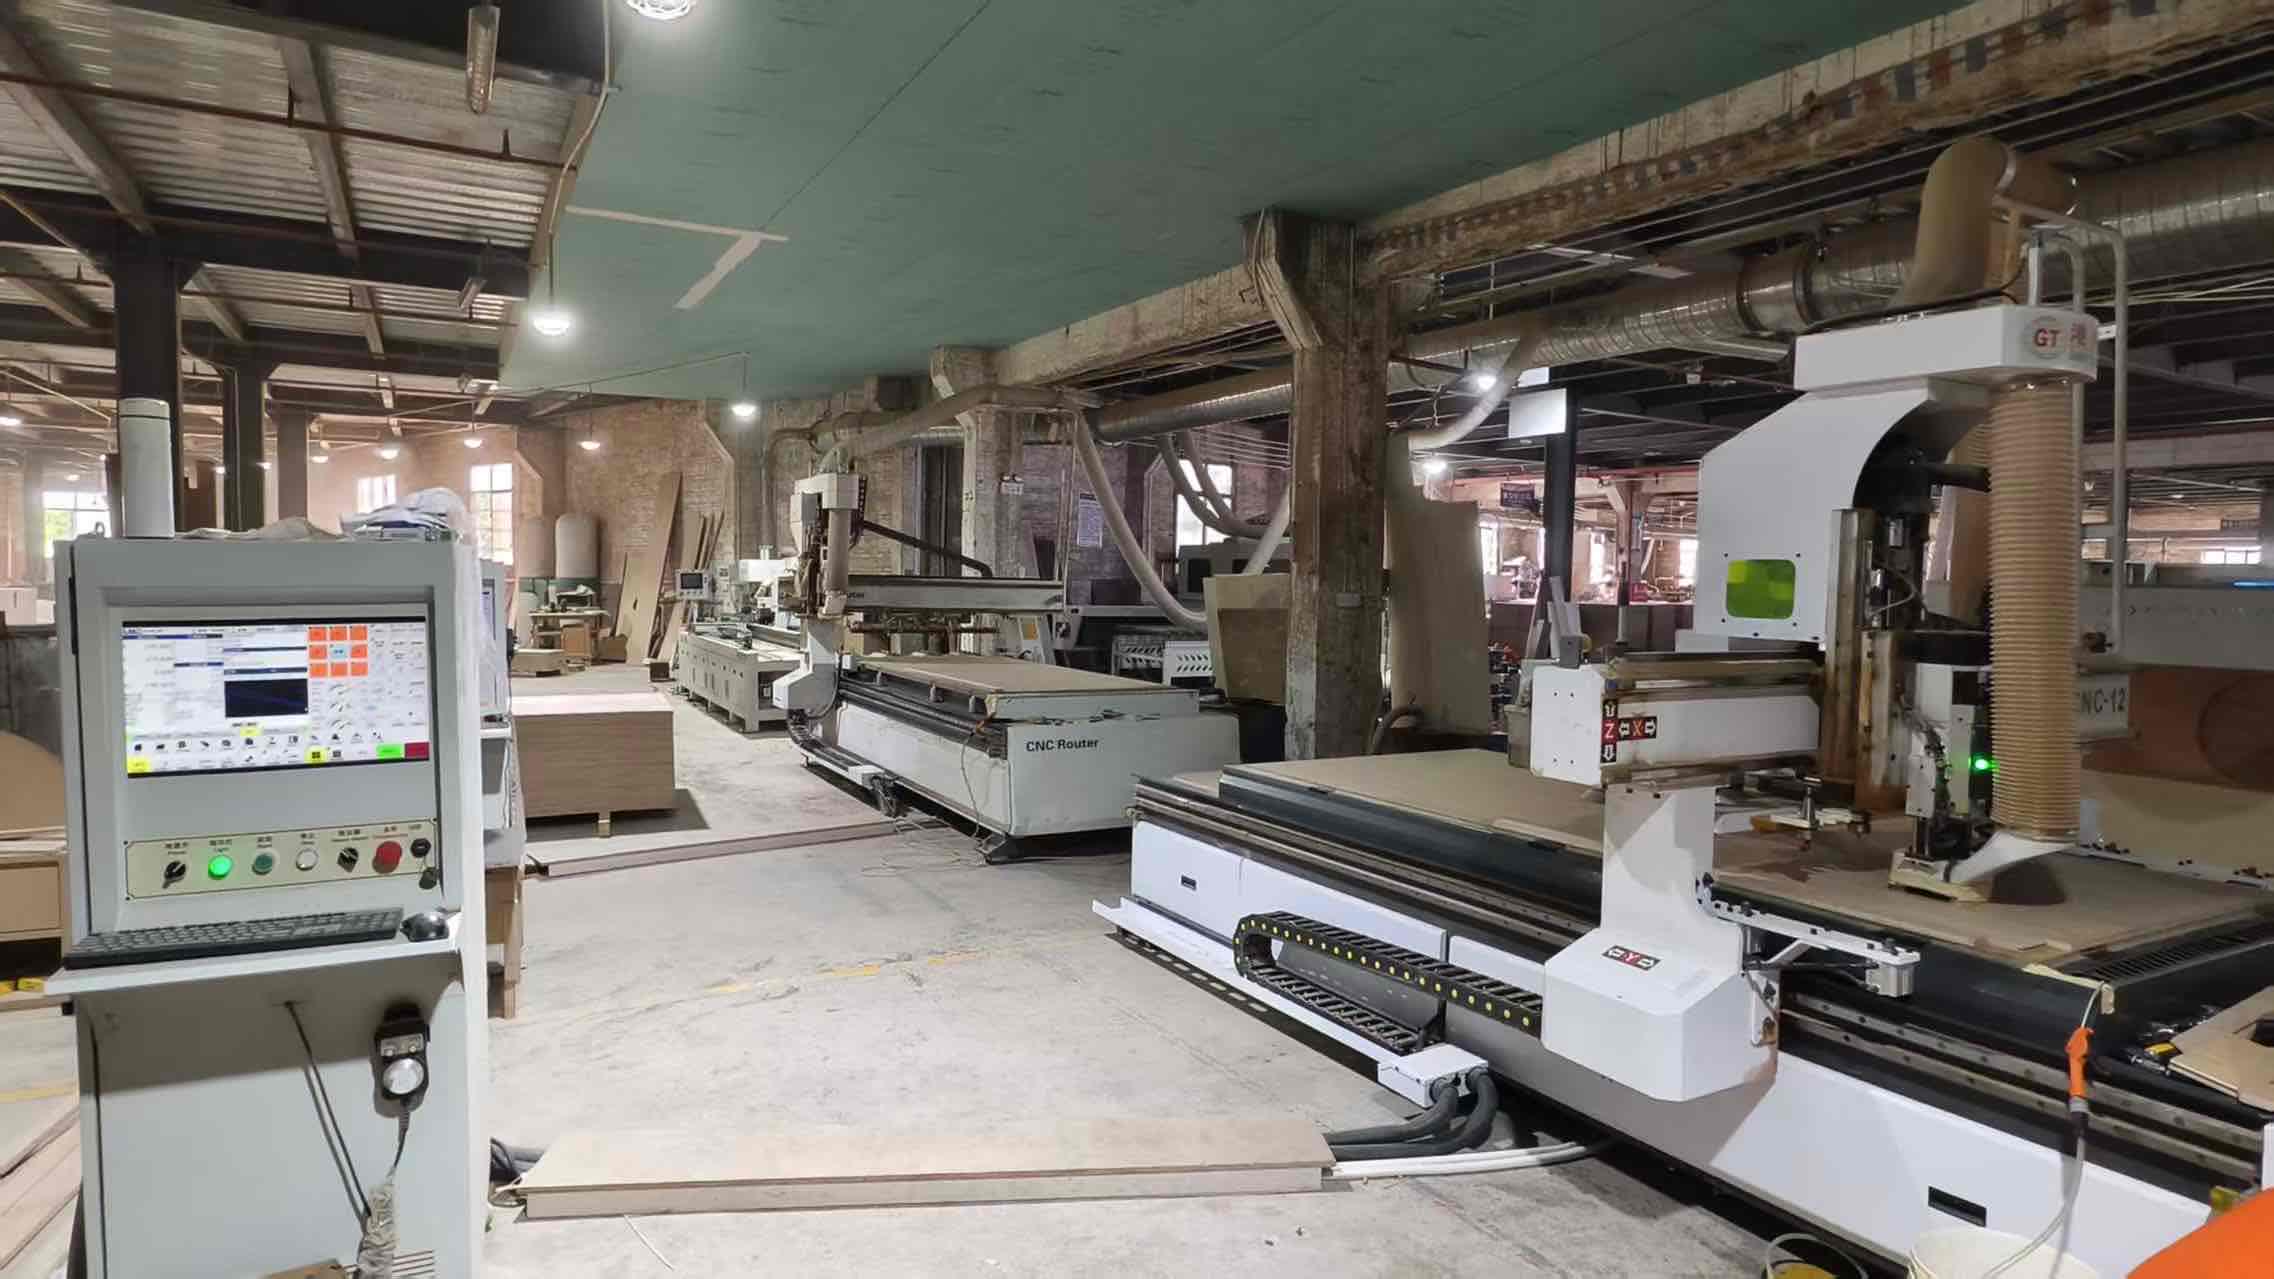
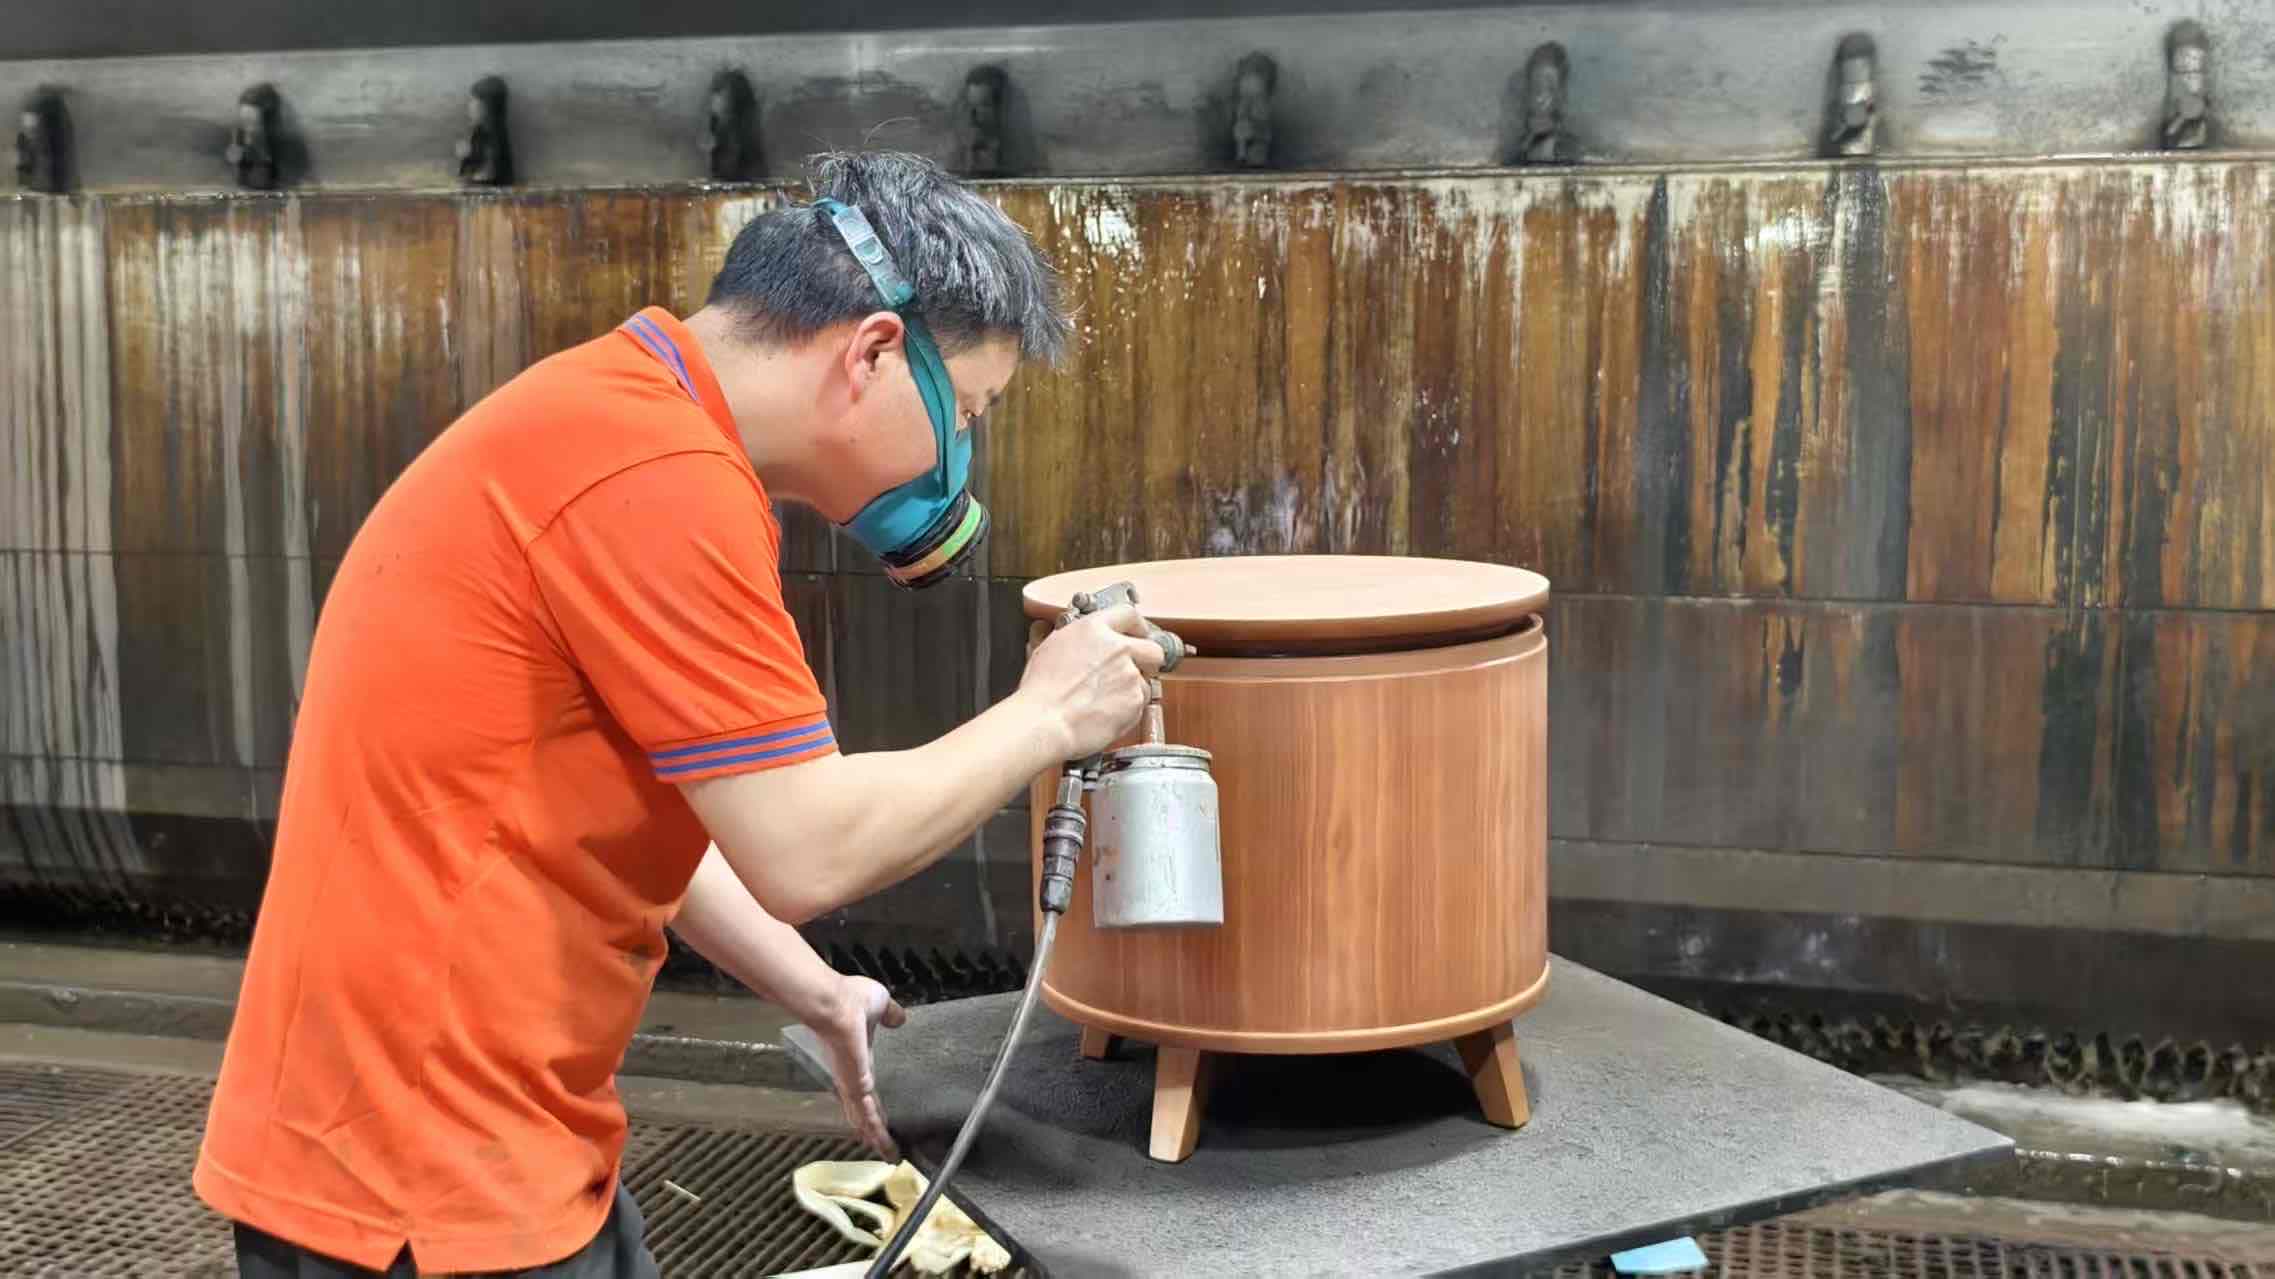
Under One Roof: The Foshan Production Facility
Independent third-party inspection, CNC machining lines, hand craftsmanship, and full-scale 1:1 project sample rooms verified on-site by SGS Group.
Factory Value Proposition
Why Global Hoteliers & FF&E Specifiers Partner with Us
Eliminating intermediaries, controlling risk at source, and delivering turnkey accountability from shop drawings to on-site assembly guidance.
Rapid Technical Drafting
Our in-house technical engineering team converts designer sketches and architectural elevation files into millimeter-accurate CAD shop drawings and joinery details within 5 to 10 working days.
Rigorous 1:1 Mock-Up Verification
Before mass fabrication begins, we fabricate a full-scale physical mock-up room in our 2,000 m² showroom within 20 days, allowing brand auditors to verify ergonomic proportions, surface sheen, and structural comfort.
Total Traceability & Floor Labelling
All items are pre-assembled and filmed for buyer sign-off, then flat-packed or pre-crated with clear identification labels indexed by room number, wing, and floor level, drastically reducing on-site staging bottlenecks.
Knowledge Base
Frequently Asked Procurement & Export Inquiries
Direct answers to questions surrounding order minimums, international certifications, logistics coordination, and bespoke production schedules.
What are the baseline minimum order quantities (MOQ) for custom guestroom packages?
+
Standard guestroom bedroom suites typically begin at a minimum batch size of 10 to 20 full sets, allowing our automated production lines to achieve optimal cutting and material yields. For dining chairs, booth seating, or public lounge components, our standard threshold is 20 units. However, for large hotel developments, we produce single-unit physical mockups (1:1 sample rooms) for technical approval prior to authorizing mass runs.
How does the factory manage fire-retardant and emission compliance across different regional codes?
+
Every export consignment is engineered to match the regulatory code of the destination country. For North American destinations, foams and cover materials are tested and certified to CAL TB 117 standards. For the United Kingdom and Middle Eastern tenders, we formulate configurations to BS 5852 Crib 5 flammability standards. In addition, all engineered timber panels adhere to E0 or CARB P2 formaldehyde emission thresholds, confirmed through routine third-party SGS/TÜV documentation.
What is the typical end-to-end timeline from design freeze to container loading?
+
Our standard workflow spans roughly 45 to 60 calendar days. Shop drawing formulation and material approval take 5 to 10 days. The physical 1:1 mock-up verification requires approximately 20 days. Once client sign-off is logged, mass fabrication, multi-stage finishing, pre-assembly inspection, and crating are completed in 45 days. Phased shipping programs can be arranged for multi-tower projects opening across staggered schedules.
Do you offer on-site installation guidance or overseas project deployment?
+
Yes. Depending on contract scope and project logistics, we deploy senior site supervisors and installation engineers to the property location. Our engineers oversee uncrating, coordinate with local trade unions or mechanical contractors, and direct the precision leveling and wall anchorage of large headboard structures and casegoods. Comprehensive, CAD-indexed instruction manuals are provided for all modular components.
Can you produce custom pieces to strict international hotel brand standards?
+
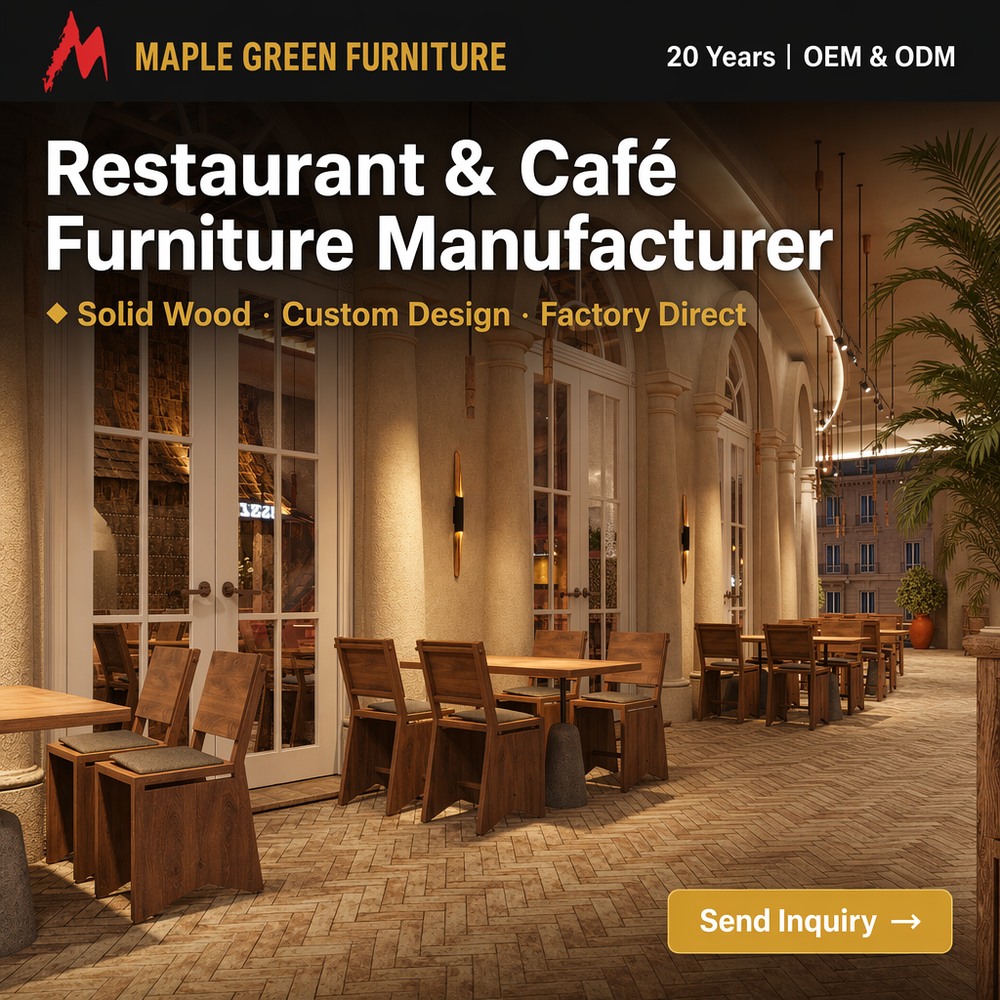
Yes. Over our 20-year manufacturing history, we have delivered custom FF&E manufactured to the design and quality guidelines of properties operating under major international flags, including Marriott, InterContinental, and boutique independent operators. We work fluidly from architectural design tenders, BIM models, elevation renderings, or physical control samples to match specified sheen, veneer cut, and hardware requirements.
Plan Your Next Hospitality Project with a Direct Manufacturer
Connect directly with our senior project engineering desk. Submit your FF&E schedule, architectural elevations, or tender requirements to receive comprehensive engineering feedback, value-engineering suggestions, and a formal cost analysis.