Engineered Contract Furnishings for 3-Star to 5-Star Hospitality Real Estate
From architectural CAD shop drawings and full-scale 1:1 guestroom mockups to automated CNC veneer joinery and on-site global installation guidance, Foshan Daski Furniture delivers seamless end-to-end FF&E procurement solutions built to brand-standard specifications worldwide.
Featured Hospitality Casegoods & Commercial Seating Sets
Explore eight of our benchmark hotel guestroom, apartment, and dining suite packages engineered specifically for intensive hospitality duty cycles, moisture durability, and commercial fire rating codes.
 Ash Wood Series
5 Star Hotel Room Furniture Package Complete Set Ash Wood Eco-Friendly Custom Luxury Modern Fire Retardant Apartment 10-Year
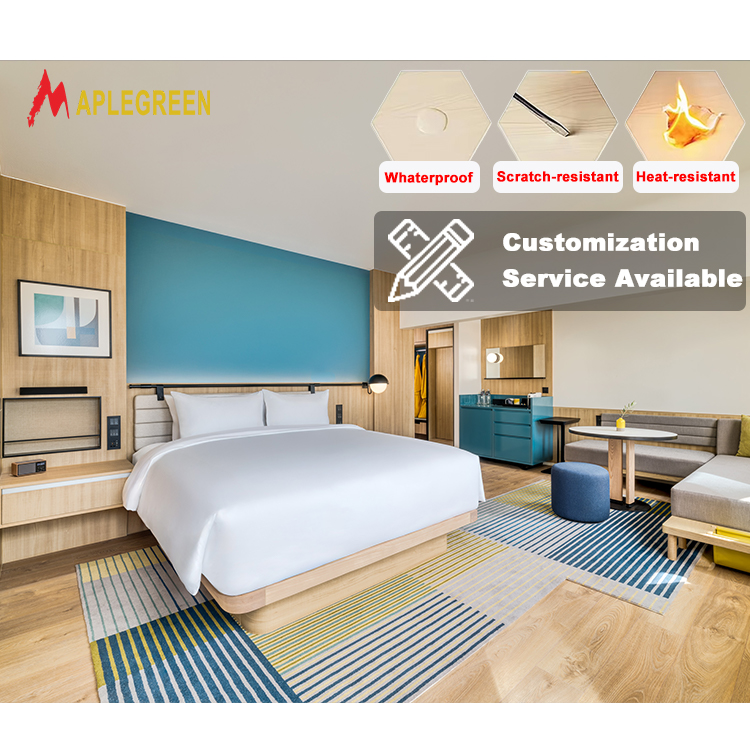 5-Star Luxury
Custom Luxury Modern Solid Wood Durable Hotel Bedroom Furniture Set for 5 Star Hotels Apartments 10 Year Warranty
 Eco-Certified
Hotel Bedroom Furniture Set Solid Wood Eco-Friendly 10 Year Warranty Ready Ship Custom Modern Design Luxury 5 Star Apartment
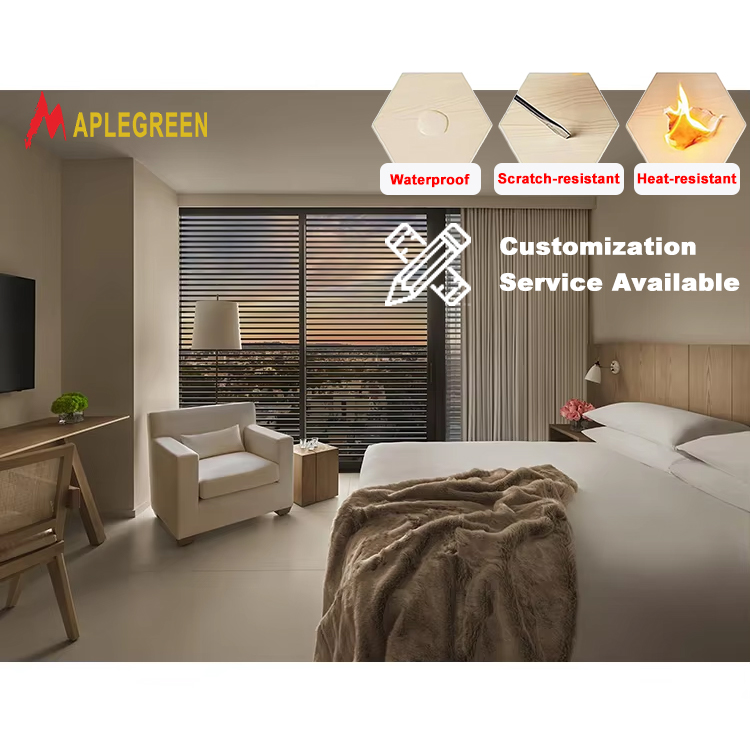 Villa & Multi-Family
Modern Wood Hotel Bedroom Set with MDF Panel Design Eco-Friendly & Water Resistant for Apartment Villa Use-Commercial Furniture
 Brand Standard Spec
Hotel Bedroom Furniture Set InterContinental Hotel Custom Modern Design Luxury 5 Star Room Solid Wood Eco-Friendly Apartment 10
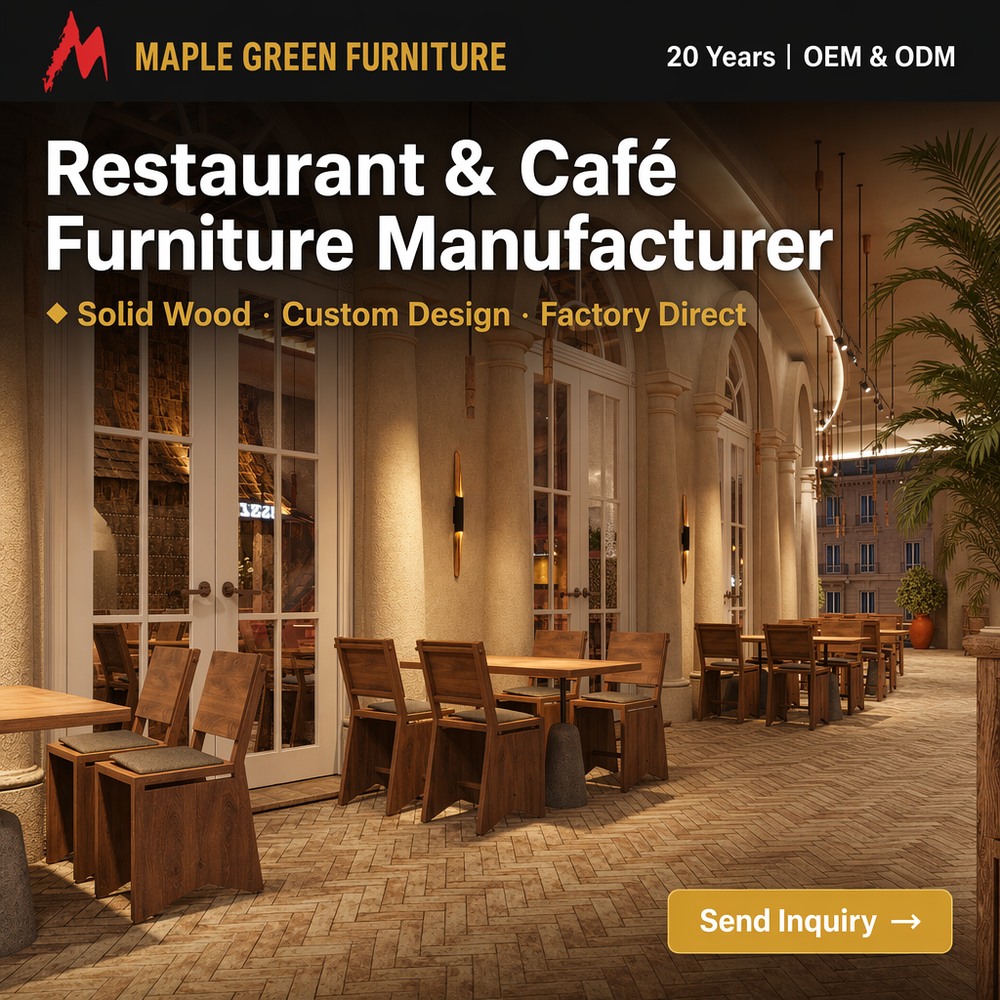 F&B Commercial Seating
Modern Solid Wood Restaurant Dining Table Chair Set Custom Booth Seating Commercial Hotel Cafe Furniture
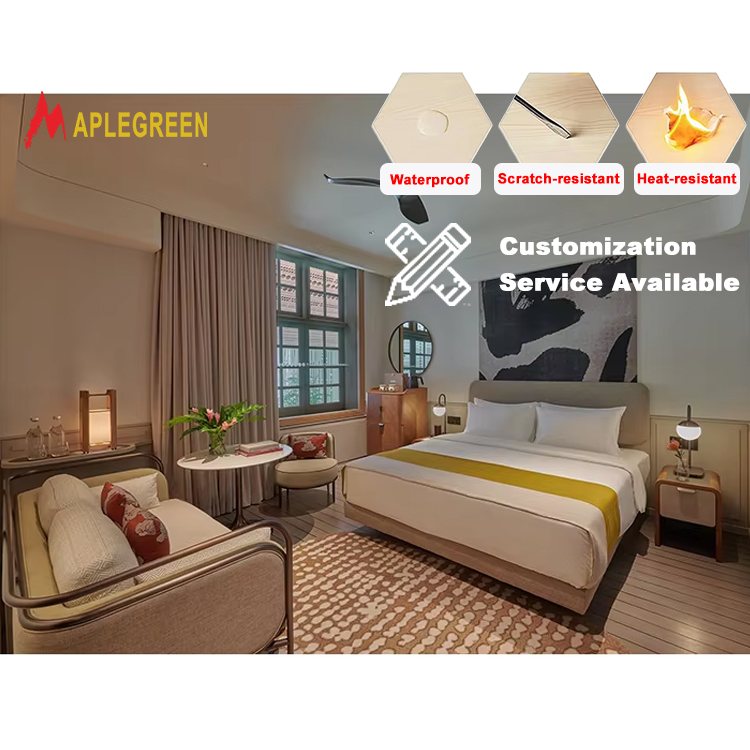 Executive Suite Suite
Modern Luxury Marriott Hotel Bedroom Set 5 Star Design Solid Wood Hotel Furniture for Villa and Apartment Commercial Use
 Turnkey Casegoods
Luxury Solid Wood Hotel Bedroom Furniture Set for 3-5 Star Hotels Apartments Modern Custom Design OEM Supplier 10 Year Warranty
Strategic Hospitality FF&E Procurement: Balancing CapEx, Lead Time, and Brand Compliance
Sourcing bespoke hotel casegoods, upholstered seating, and public-area millwork requires balancing aesthetic intent, engineering durability, and capital expenditure constraints. Hospitality furniture experiences duty cycles five to eight times heavier than domestic residential items. A luggage drop on an unprotected veneer edge, frequent thermal shock from guestroom beverage stations, and repeated industrial chemical wipe-downs quickly degrade sub-standard finishes. As an authentic Foshan custom hotel furniture manufacturer operating continuously since 2004, Foshan Daski Furniture Co., Ltd. eliminates systemic failure modes by engineering every piece from internal sub-frames outward.
Our direct OEM/ODM infrastructure bridges the gap between interior design firms and on-site contractors. By maintaining our own 28,000 square meter manufacturing plant equipped with multi-axis CNC routers, automated veneer press machinery, specialized spray-finishing rooms, and dedicated pre-assembly dry-fit zones, we enforce rigorous quality gate controls at every juncture. Whether matching exact brand standards for Marriott, Hilton, or InterContinental franchises, or developing value-engineered alternatives for independent boutique resort developers, our single-facility workflow ensures absolute traceability from raw timber kiln-drying to export container loading.
Why Global Hoteliers & Procurement Firms Rely on Daski
By eliminating sourcing intermediaries and managing all custom millwork and upholstery production in-house, Daski delivers verifiable cost reductions, uncompromising quality compliance, and reliable scheduling for international projects.
28,000 m² Integrated Manufacturing Hub
Located in Jiujiang, Foshan—China's global capital for contract furniture production—our plant combines heavy wood processing, precision veneer lamination, custom metal hardware fabrication, and high-density upholstery workshops under one central engineering team.
- Zero subcontractor hand-offs or split liabilities
- Full custody chain tracking from lumber to crate
- Direct access to Foshan's prime material supply chain
Rapid Shop Drawings & Value Engineering
Our dedicated drafting department translates designer schematics and ID renderings into millimetre-accurate AutoCAD/SolidWorks shop drawings within 5 to 10 days, proactively flagging potential structural vulnerabilities and optimizing material yield to lower CapEx.
- Smart joint construction and edge-banding details
- Power, USB, and LED integration engineering
- Direct value-engineering trade studies
Full-Scale 1:1 Sample Mockup Rooms
We eliminate guesswork before mass production by building a complete 1:1 model room in our dedicated mockup workshop within approximately 20 days. Clients and brand inspectors can test physical comfort, view finishes under real lighting, and inspect dry-fit tolerances.
- Physical validation of proportions and ergonomics
- Finish sample chips and hardware sign-off
- Pre-shipment video conferencing and approval
Stringent International Fire & Eco Standards
Every commercial furnishing package is built to comply with destination country codes. From North American CAL TB 117 and British Standard BS 5852 fire resistance to European E0/E1 low-formaldehyde panel ratings, our factory provides authentic lab certification documents.
- ISO 9001 certified quality management protocols
- On-site verified assessment by SGS Group
- Eco-friendly multi-layer polyurethane coatings
Export-Grade Protection & Site Distribution
Damage at destination halts project timelines. Daski uses 5-layer heavy corrugated cartons with custom-molded pearl-cotton (EPE) corner protectors and fumigated plywood crating. Goods are labeled room-by-room and floor-by-floor for streamlined site staging.
- Drop-tested packaging engineered for sea freight
- Detailed container loading plans and packing lists
- Floor-specific barcoded identification tags
Global Engineering & Installation Guidance
Our commitment extends beyond port delivery. We provide comprehensive step-by-step 3D assembly guides, numbered hardware diagrams, and, upon request, can dispatch senior bilingual installation engineers directly to your job site anywhere in the world.
- On-site supervision of local millwork subcontractors
- Resolution of field dimensional discrepancies
- Turnkey installation packages for full-service openings
A 5-Stage Engineering Protocol for Predictable Delivery
Hospitality construction deadlines are unforgiving. Our systematic gate-review process ensures clear project milestones, transparent design approvals, and dependable 45-day mass manufacturing lead times.
Shop Drawings & Review
5–10 Calendar DaysTranslating BOQ and schematics into detailed fabrication drawings with joinery, material callouts, and hardware specifications.
1:1 Mockup Production
≈ 20 Days DurationPhysical sample room fabrication allowing owners, operators, and interior designers to evaluate ergonomics, finishes, and construction.
Compliance Auditing
Material Gate ReviewRigorous moisture checking of natural timbers, flame-retardant fabric testing (CAL 117/BS 5852), and laminate edge-pull inspections.
Trial Dry-Fit Assembly
Video DocumentedFull pre-assembly of complete casegoods and headboard panels in our workshop to ensure seamless site fit-up prior to export packing.
Mass Run & Logistics
45-Day Standard LeadAutomated batch processing, multi-point QC stamping, floor-coded crating, container load optimization, and global ocean forwarding.
Future Procurement Trends: Where Modern Hospitality FF&E Is Headed
Procuring commercial hotel furniture is shifting toward stricter life-cycle costing, circularity, and smart-room integration. Forward-thinking owners and hotel asset managers are no longer prioritizing initial purchase price over long-term durability. Instead, procurement strategies focus on minimizing operational disruption during mid-cycle renovations.
1. Modular Architectural Millwork: Rather than permanently affixed wall paneling that requires destructive demolition to remodel, operators demand demountable cleat-hung headboard walls with modular upholstery inserts. When soft goods soil or wear out after four to five years, maintenance teams can unclip and re-upholster individual panels overnight without taking guestrooms out of inventory.
2. Concealed IoT and Wireless Power Infrastructure: Bedside nightstands, executive writing desks, and public lounge banquettes now integrate discreet Qi2 fast wireless charging pads, flush AC/USB-C PD high-output power ports, and indirect 2700K warm LED accent channels. Modern factory drawings must treat hotel furniture as an architectural electrical conduit housing safe, ventilated wiring chases.
3. Ultra-Durable Low-VOC Surface Technologies: Natural wood veneers remain the luxury benchmark, but hotel brands increasingly require advanced hybrid finishes: micro-thin open-pore waterborne polyurethanes, ceramic-infused scratch-resistant top coats, and sintered stone or anti-fingerprint compact laminate (Fenix/HPL) tops for high-touch desks and luggage benches.
4. Verified Circularity and Scope 3 Emissions: ESG and LEED/BREEAM green certifications have moved to the center of institutional hospitality development. Institutional investors mandate verified E0/CARB P2 composite cores, certified sustainable timber sources (FSC/PEFC), non-hazardous water-based adhesives, and fully recyclable crating materials.
Technical Hospitality FF&E Specification Matrix
Use this reference table to align project architectural specifications with factory production capabilities and international contract compliance standards.
| FF&E Category | Primary Substrate & Frame | Surface Finish & Veneer | Hardware & Mechanics | International Compliance Standards |
|---|---|---|---|---|
| Hotel Guestroom Suites | Kiln-dried solid ash/beech framing + E0/E1 moisture-resistant MDF/plywood core | Natural walnut, oak, or ash veneer (0.6mm thickness) with 5-coat PU finish | DTC/Blum soft-closing concealed hinges, heavy-duty undermount ball slides | CARB Phase 2, EPA TSCA Title VI, E0 formaldehyde emissions, ISO 9001 |
| Fire-Rated Headboards | Engineered hardwood structural skeleton with sound-dampening acoustic core | Stain-shield performance fabric, commercial faux leather, or top-grain leather | Heavy-gauge Z-clip French cleat concealed steel wall mounting system | CAL TB 117 (USA), BS 5852 Crib 5 (UK/EU), NFPA 260 flammability ratings |
| Restaurant Booth Seating | Reinforced kiln-dried birch timber with glued, screwed, and corner-blocked joints | Heavy-traffic commercial vinyl or woven upholstery (>100,000 Wyzenbeek rubs) | High-resilience foam core (45-50 kg/m³) with serpentine spring under-structure | BS 7176 Medium Hazard, CAL 133 barrier compliant, antimicrobial coatings |
| Public Lobby Lounge Sets | Welded 304 stainless steel interior chassis or high-density curved birch plywood | Custom PVD titanium electroplated metal bases with plush contract velvets | Industrial non-marking floor glides, structural tie-rod reinforcement | BIFMA X5.4 lounge seating standards, ISO 14001 environmental management |
| Luggage Benches & Desks | Multi-layer marine-grade plywood substrate with solid wood protective perimeter | Sintered stone, engineered quartz, or high-pressure laminate (HPL) desktop insets | Integrated brush grommets, hidden cable trays, flush-mounted USB/AC sockets | Scratch test grade 4H, water-resistant boiling test standard, UL listed wire routing |
Frequently Asked Questions on Custom FF&E Procurement
Direct, actionable answers to common technical, logistics, and scheduling questions asked by commercial hotel developers, purchasing managers, and general contractors.
Q1: What is the factory minimum order quantity (MOQ) for custom hospitality casegoods?
Our standard production MOQ for custom guestroom bedroom sets is typically 10 to 20 complete keys (sets), allowing efficient board yield and CNC machining optimization. For restaurant chairs, barstools, and booth seating, MOQs start at 20 pieces. We also support single-piece prototypes and full 1:1 guestroom mockups before signing off on mass production orders.
Q2: How does Daski ensure timber stability and prevent veneer cracking in high-humidity climates?
We source premium kiln-dried hardwoods and run them through our computerized balance kilns to stabilize moisture content between 8% and 12%, matched to your project's local climate. Veneered panels receive matching backing veneers to equalize surface tension, and core edges are sealed with polyurethane barriers to block ambient humidity and prevent delamination.
Q3: Can you manufacture furnishings strictly to international brand standards (Marriott, Hilton, IHG)?
Yes. Our engineering department regularly produces furniture to rigorous brand design guides and technical specifications. We accommodate exact joinery details, specified commercial hardware (such as Blum or Hafele), branded aesthetic profiles, and provide fire-rated, low-emission material test certificates for corporate sign-off.
Q4: What is the typical end-to-end timeline from project quotation to container departure?
Our typical workflow runs on a dependable timeline: CAD shop drawings take 5 to 10 days; a 1:1 sample room takes approximately 20 days; and standard mass production runs 45 days after sample and deposit approval. Total turnkey production usually wraps within 60 to 75 days, excluding ocean freight transit times.
Q5: What flammability and emission documentation do you supply for building inspectors?
We supply official laboratory testing reports for CAL TB 117 and British Standard BS 5852 Crib 5 fire-retardant upholstery foams and fabrics. For wood composite cores, we supply E0, E1, CARB Phase 2, and EPA TSCA Title VI test certificates to ensure compliance with local building authorities and green building protocols.
Q6: How are fragile marble, glass, and long casegoods protected against rough ocean handling?
All items undergo a six-tier packaging process: protective PE film, high-density EPE pearl-foam corner protectors, edge guards, heavy-duty 5-layer corrugated cartons, and custom-built fumigated plywood crates for stone, glass, and high-gloss surfaces. Boxes are labeled with room numbers, floor levels, and handling barcodes for organized site staging.
Q7: Do you provide on-site installation support for overseas hotel openings?
Yes. In addition to delivering detailed 3D exploded assembly diagrams and video walk-throughs, Daski can dispatch senior installation supervisors and bilingual project engineers directly to your job site to guide local labor crews, troubleshoot building variances, and inspect final fits before hotel handover.
Q8: How does your factory handle design revisions or field dimension changes mid-project?
Before cutting raw boards, our shop drawing review phase includes checking dimensions against as-built site conditions. If plumbing, structural columns, or drywall offsets require adjustments, our engineering team updates the CAD models, documents any scope adjustments transparently, and re-issues approval sheets before machining begins.
Bring Your FF&E Schedule to Life with Direct Factory Pricing
Whether you need a full five-star hotel casegoods package, custom restaurant booth seating, or a full 1:1 guestroom mockup, our engineering and estimating team is ready to review your architectural drawings and Bill of Quantities.