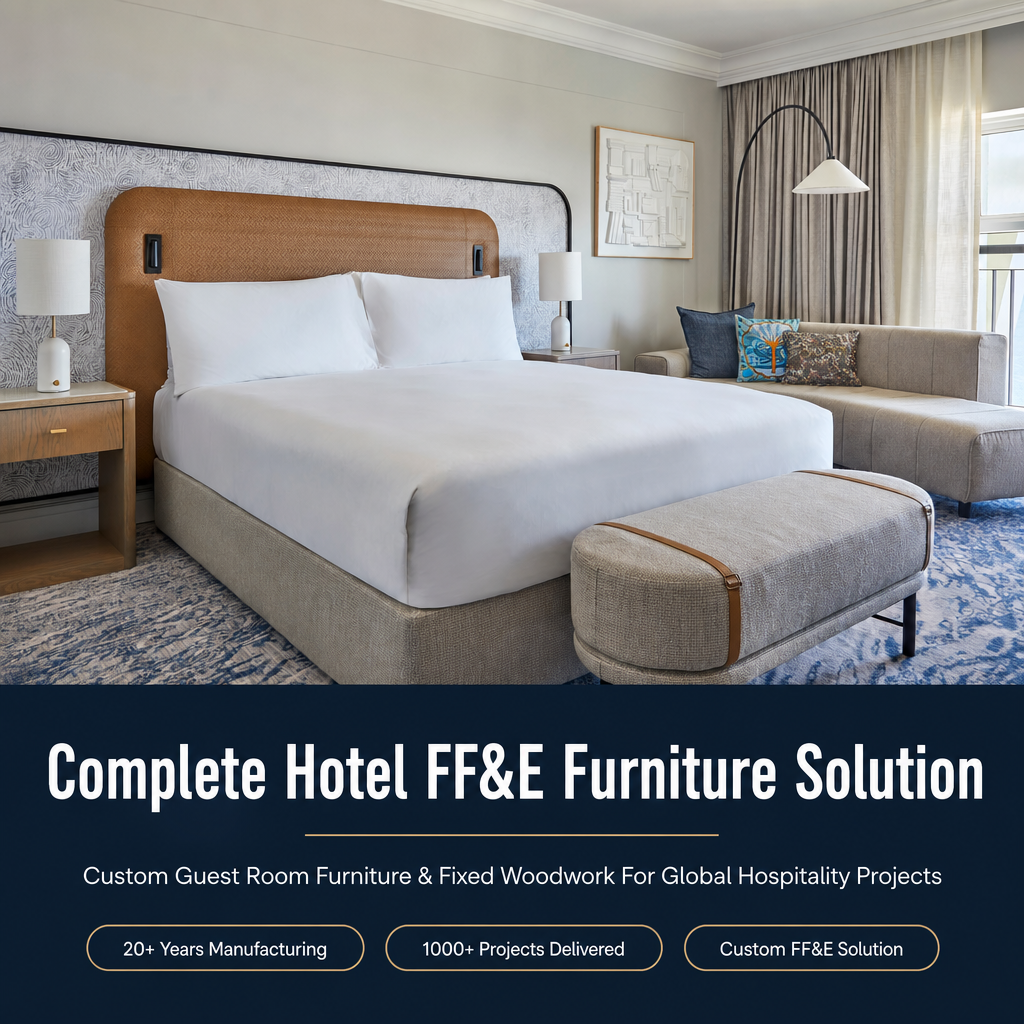
Direct Factory Production
Engineered Hotel Bedroom Sets & Storage Collections
From integrated master wardrobes and smart luggage consoles to fire-rated nightstands and hospitality casegoods, browse our OEM/ODM custom solutions built for tier-1 hospitality developments.
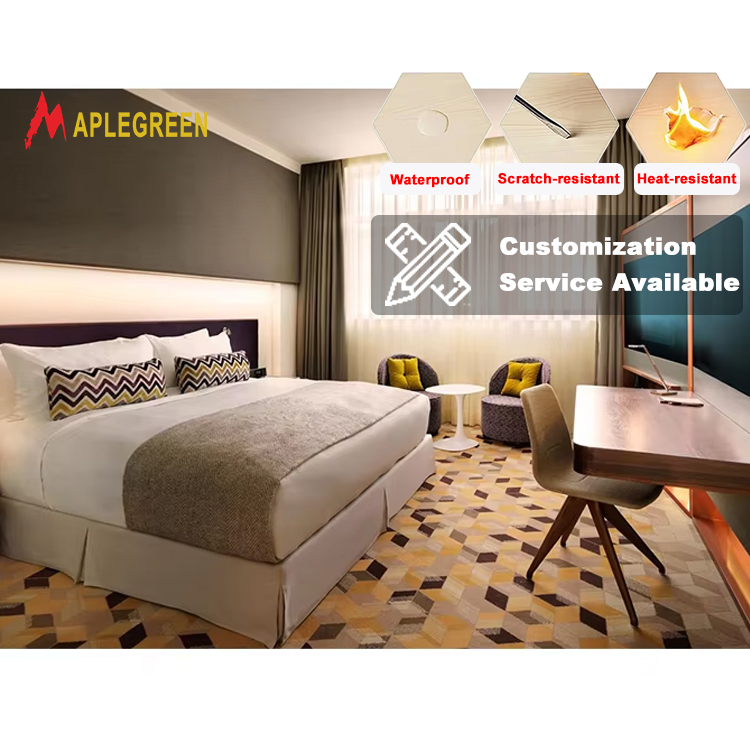
Industrial Scale & Capacity
Audited Production Capabilities Built on 20+ Years of Craft
Located in Jiujiang, Foshan—the core epicenter of world hospitality manufacturing—our vertically integrated facility guarantees direct factory pricing, zero subcontracting dilution, and complete material traceability.
2004
Founded Year
28,000㎡
Production Floor
2,000㎡
Sample Showroom
200+
Master Craftsmen
1,000+
Projects Fitted
45 Days
Standard Lead Time
Rapid Shop Drawings
CAD and engineered 3D production blueprints finalized within 5 to 10 days to eliminate architectural discrepancies before production begins.
1:1 Mock-Up Suite
Full 1:1 scale sample guestroom fabricated within 20 days for owner sign-off, tactile comfort evaluation, and joint stress verification.
Global Fire Ratings
Compliant with CAL TB 117 (US) and BS 5852 Crib 5 (UK) fire retardancy standards, alongside E0/E1 low-formaldehyde board emissions.
Pre-Assembly & Traceability
100% pre-assembly inspection before factory export, complemented with floor-by-floor and room-by-room labeled packaging for rapid overseas setup.
Strategic Procurement Intelligence
Future Procurement Trends in Hospitality Bedroom Storage
Procurement executives, interior designers, and real estate developers are restructuring FF&E guidelines to address shifting consumer habits, life-cycle costs, and strict ESG compliance standards.
Open-Concept Wardrobe Architecture
Traditional, heavy enclosed armoires are being rapidly replaced by minimalist open storage frameworks, metallic hanging rods, and integrated luggage landing benches. This layout expands guest visibility, prevents forgotten personal belongings, reduces turn-time for housekeeping, and cuts panel raw material costs by up to 25% without sacrificing elegance.
Concealed Smart Tech & Power Integration
Modern guestroom storage now incorporates wire management, wireless inductive charging ports, biometric safe enclosures, and concealed linear warm-LED strip illumination (2700K–3000K). Casegoods factories must possess advanced internal routering capabilities to integrate sensors that automatically trigger interior illumination when cabinet drawers or wardrobes slide open.
Modular FF&E & Life-Cycle Value Engineering
Hotel developers prioritize high-pressure laminate (HPL) surface tops and solid wood edge-bandings over vulnerable all-lacquer profiles. Replaceable headboard panel sections, modular drawer cassettes, and reversible nightstand compartments safeguard brand aesthetics against heavy luggage impacts while extending the renovation cycle from 5 to 8+ years.
Engineering Innovations
Technological & Material Evolution in Hotel Storage
Examine how state-of-the-art CNC precision joinery, advanced moisture mitigation, and circular construction frameworks are defining the next generation of contract-grade hotel casegoods.
Climate-Adaptive Moisture Engineering
For resort and coastal installations across the Middle East, Florida, and Southeast Asia, casegoods face extreme humidity shifts. Modern manufacturers calibrate kiln-dried solid timber (moisture content strictly stabilized at 8%–12%) and utilize multi-layer water-resistant polyurethane sealing primers to inhibit structural warping, veneer blistering, and joint separation.
Heavy-Duty Contract Hardware Systems
Residential drawer runners fail under commercial hotel turnover. The industry standard has transitioned toward heavy-gauge concealed under-mount soft-close glides (tested to 50,000+ cycle open/close fatigue runs), 110-degree institutional hinges with integrated dampers, and 304 stainless steel luggage protector strips that defend surfaces from wheel abrasions.
Low-VOC Waterborne Finishes & LEED Compliance
International environmental regulations have accelerated the adoption of electrostatic waterborne UV coatings and zero-emission E0/carb-phase-2 compliant substrate cores. These finishes eliminate noxious off-gassing upon delivery, allowing newly fitted hotels to achieve immediate guest occupancy without lingering chemical odors while earning LEED credits.
Buyer Knowledge Base
Frequently Asked Questions on Hotel Storage Procurement
Direct answers to the critical technical, operational, and logistic inquiries encountered by hospitality purchasing directors, general contractors, and specifiers.
Our standard production runs for custom hotel bedroom suites and integrated wardrobe systems start at 10 to 20 guestroom sets. For boutique properties or specialized design testing, single-room 1:1 prototype mock-ups can be produced and fully evaluated prior to activating the full bulk manufacturing schedule.
Our project management protocol operates in 5 structured phases: (1) CAD shop drawings and value engineering sign-off in 5–10 days; (2) 1:1 physical sample suite fabrication in approximately 20 days; (3) Raw material compliance verification; (4) Pre-assembly and dimensional stress testing with video documentation; (5) Full mass production across 45 standard days, followed by room-specific export crating.
We routinely build to North American CAL TB 117 flammability criteria and British Standard BS 5852 (Crib 5) requirements for hospitality upholstery, foam, and headboard elements. All engineered wood cores, veneers, and backing panels can be specified to CARB Phase 2, EPA TSCA Title VI, or European E0/E1 low-formaldehyde emission standards.
Yes. Our engineering division operates as an OEM/ODM manufacturing partner for brand-approved casegoods across Marriott, Hilton, IHG, and Wyndham specifications. We manufacture directly from brand standard design intent books, project FF&E schedules, or bespoke architectural renderings, preserving strict color balance, grain direction, and hardware specifications.
All casegoods feature high-density PE foam corner protectors, multi-layer scratch-resistant pearl cotton wrapping, edge guards, and heavy-duty 5-ply corrugated export cartons. High-risk elements such as natural marble tops, tempered glass shelving, and LED mirror panels are packed in fumigated, heat-treated reinforced plywood crates marked with orientation indicators.
Yes. We provide comprehensive installation documentation, hardware layout plans, and exploded 3D assembly guides with every consignment. Upon request, our senior engineering directors can travel directly to your hotel project site to oversee general contractor assembly or dispatch experienced factory installation teams for full turn-key execution.